Over 50,000 hot-selling automation module components.

ABB CI867 Modbus TCP Zero-Data Fix & Byte Swap Guide

Troubleshooting ABB CI867 Modbus TCP Zero-Data Faults and Byte Swap Issues After Module Replacement

Replacing an industrial communication interface in a distributed control system (DCS) often presents unexpected challenges. Maintenance teams frequently observe that replacing an ABB CI867 Modbus TCP module results in all field data displaying zero. However, the physical Link LED on the Ethernet port shows normal operation. Powergear X Automation provides this troubleshooting guide to resolve data integrity issues in ABB System 800xA and AC 800M control systems.
Distinguishing Physical Ethernet Connectivity from Modbus Application Integrity

A solid Link LED indicates a healthy physical Layer 1 Ethernet connection. However, physical layer stability does not guarantee correct application layer data exchange. Modbus TCP operates as a client-server protocol requiring precise register mapping and matching data formats. According to industrial networking surveys, over 40% of post-replacement field errors stem from software configuration mismatches rather than hardware defects. Therefore, engineers must separate physical connectivity from data interpretation when diagnosing all-zero readings.

Understanding Byte Swap and Word Swap Dynamics in Process Automation

Modbus TCP transmits 16-bit register pairs using standard big-endian byte ordering. However, multi-register 32-bit values like floating-point numbers require careful byte and word alignment. Swapping high and low bytes alters integer values within a single 16-bit word. Conversely, word swapping exchanges the positions of two adjacent 16-bit registers. While a byte swap mismatch generates incorrect numerical values, it rarely causes every register to read zero simultaneously.

Identifying Root Causes of All-Zero Readings in Factory Automation

When every Modbus register displays zero after module replacement, investigate underlying configuration mismatches. Common causes include incorrect starting register addresses, offset errors, and unsupported Modbus function codes. For instance, requesting Function Code 03 instead of Function Code 04 can cause quiet read failures. In addition, uninitialized application variables or missing communication status flags force PLC and DCS logic to output zero values for safety.

Step-by-Step Commissioning Sequence for CI867 Module Integration

  1. Verify Physical Communication: Confirm active IP configuration, subnet masks, and ping connectivity between the CI867 and remote devices.
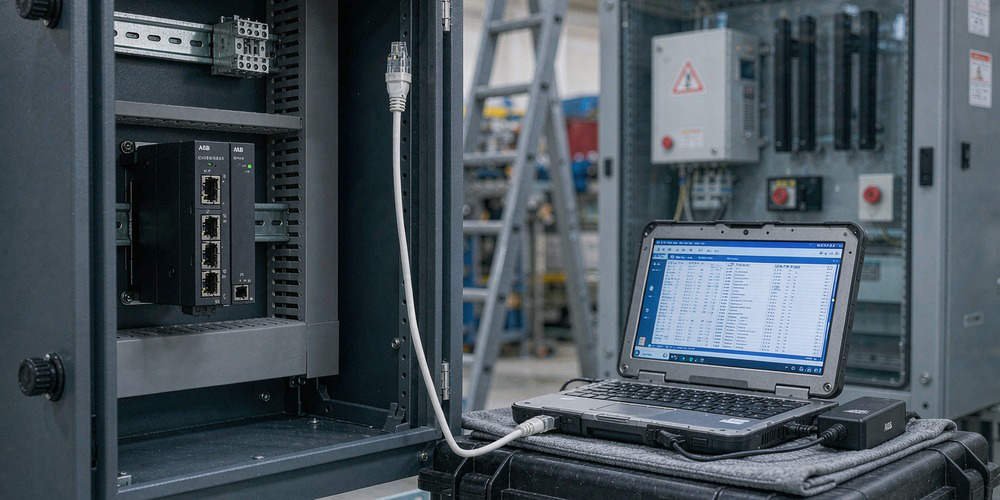
  2. Capture Raw Register Data: Use Control Builder software or a Modbus poll utility to inspect unformatted hexadecimal register values.
  3. Validate Register Addressing: Verify whether the field instrument utilizes zero-based or one-based Modbus register addressing.
  4. Check Byte Order Settings: Compare raw register hex codes against documented field device values before enabling software byte-swapping functions.
  5. Confirm Application Logic: Ensure communication status bits enable data transfer blocks within the AC 800M controller program.

Field Installation Standards and Compliance Practices

Robust field installation prevents intermittent data corruption in factory automation networks. Signal cables must maintain proper separation from high-voltage motor wiring to prevent electromagnetic interference. Furthermore, control cabinet installations must adhere to international grounding regulations under IEC 61000 standards. Engineering teams must document all firmware revisions and Control Builder settings prior to performing hardware maintenance.

B2B Procurement and Hardware Compatibility Insights

Procurement specialists must verify hardware revisions and firmware compatibility when purchasing replacement parts. Modern CI867A modules offer enhanced diagnostics but require specific System 800xA software versions. Simply matching a base part number does not guarantee seamless hot-swapping without configuration updates. Therefore, integration teams should validate firmware compatibility before installing spare parts during planned downtime.

Application Scenario: Refined Chemical Processing Line

A chemical plant replaced a faulty CI867 module connecting an AC 800M DCS to a rack of variable speed drives. Following the replacement, all motor speed and current feedback values dropped to zero, halting production interlocks. The Ethernet Link LED remained fully operational, leading technicians to suspect a corrupt drive program.

Engineers from Powergear X Automation inspected the system and discovered that the replacement module defaulted to Function Code 04 (Input Registers), whereas the drives required Function Code 03 (Holding Registers). Reconfiguring the Control Builder hardware tree restored raw communication instantly. A minor byte-swap adjustment on 32-bit float channels then returned accurate motor current readings within 30 minutes.

For certified spare parts and expert technical support on ABB AC 800M systems, visit Powergear X Automation to secure reliable hardware solutions for your plant infrastructure.

Frequently Asked Questions (FAQ)

Q1: Does a normal Link LED mean the CI867 module is transmitting Modbus data?
No. The Link LED only confirms physical layer connection to the network switch. It does not verify IP routing, Modbus TCP handshakes, or valid register polling.

Q2: How do I determine whether I need a Byte Swap or a Word Swap?
Examine raw hexadecimal data from a known non-zero register. If the individual bytes within a 16-bit register are reversed, apply a byte swap. If two adjacent registers in a 32-bit float are transposed, apply a word swap.

Q3: Can I drop a replacement CI867 module into an existing rack without software configuration?
While the CI867 supports module replacement, the hardware revision and firmware version must match the Control Builder project requirements. Always verify project settings and firmware compatibility before commissioning.
Replace ABB PP835A HMI with Third-Party OPC Touchscreens

Replacing Damaged ABB PP835A HMI with Third-Party Touchscreens via OPC Communication

Physical damage to an ABB PP835A touchscreen panel does not force plants to replace the entire DCS architecture. Operators can retain the AC 800M controller and its core control logic. By establishing an OPC communication layer, engineers can stream process variables to third-party HMIs seamlessly. Powergear X Automation presents this guide to explain how plants can maintain system stability using modern industrial automation solutions.

Understanding MMS Communication in AC 800M Control Systems

The AC 800M controller utilizes Manufacturing Message Specification (MMS) as its primary control network protocol. ABB documentation confirms that MMS handles project downloads, online diagnostics, and alarm communications. However, standard third-party HMIs cannot natively parse MMS data structures. Simply plugging an Ethernet cable into an AC 800M controller will not grant variable access. Therefore, system integrators must bridge the gap between MMS and standard Ethernet protocols.

The Role of ABB OPC Server in Protocol Translation

The ABB OPC Server for AC 800M collects field data from the controller via MMS. It then translates these values into standard OPC DA or OPC UA interfaces. As a result, third-party platforms like Siemens WinCC or Weintek HMIs can read process tags easily. This architecture protects the core control program, eliminating the need to rewrite complex controller logic. Consequently, plants save hundreds of engineering hours during panel retrofits.

Comparing OPC DA and OPC UA for Modern Plant Architectures

Legacy DCS installations heavily rely on OPC DA, which operates on Windows DCOM technology. While OPC DA offers fast local integration, it faces severe network security limitations. Conversely, OPC UA provides cross-platform compatibility, robust encryption, and built-in user authentication. Industrial automation trends show that over 70% of new factory automation upgrades now require OPC UA. Therefore, engineers should evaluate network security requirements before selecting their integration architecture.

Step-by-Step Commissioning Procedure for HMI Replacement

  1. Audit Existing Tag Sourcing: Map all process variables, data types, and alarm states from the original PP835A project.
  2. Configure Tag Access Rights: Establish read-only permissions during initial testing to protect running production equipment.
  3. Deploy Independent Test Environment: Validate OPC Server connections and tag browsing offline before connecting to the live control network.
  4. Execute Staged Variable Testing: Verify digital status indicators, analog values, and alarm quality flags prior to enabling write commands.

Field Installation Practices and Control Network Optimization

Connecting new HMIs directly to a live control network introduces unnecessary operational risks. Continuous polling of thousands of tags can overload the AC 800M Ethernet communication modules. Engineers must optimize tag update rates based on process dynamics. For instance, temperature and tank level tags require slower scan times than fast motion loops. Moreover, field technicians must follow strict isolation practices during commissioning to prevent accidental trips.

Integrating Third-Party HMIs via OPC Gateway Architecture

Deploying a dedicated OPC Gateway creates a secure buffer between the AC 800M control network and external HMIs. The gateway retrieves data via MMS and exposes encrypted OPC UA endpoints to third-party devices. Furthermore, this architecture simplifies future plant expansions, such as integrating SCADA, Historian, or MES software. As a result, plant managers achieve a modular and scalable industrial automation infrastructure.

Application Scenario: Petrochemical Facility HMI Migration

A continuous chemical processing plant suffered a screen failure on an aging ABB PP835A panel connected to an AC 800M controller. Sourcing an exact Panel 800 replacement required a four-week lead time, threatening costly plant downtime. The engineering team deployed a third-party touchscreen HMI using the existing ABB OPC Server.

First, the team created a comprehensive Tag Mapping List to mirror the original PP835A variable addresses. Second, they configured an OPC UA client interface on the new HMI to establish secure data exchange. Finally, they conducted staged read-write validation on a isolated network segment. The new HMI went live within 48 hours without modifying a single line of AC 800M controller code.

For high-performance control system components and expert technical support on DCS migrations, visit Powergear X Automation to explore reliable hardware solutions for your plant.

Frequently Asked Questions (FAQ)

Q1: Can I connect a Siemens or Weintek HMI directly to an AC 800M without an OPC Server?
Direct Ethernet connections generally fail because standard HMIs lack native AC 800M MMS protocol drivers. You must use an ABB OPC Server, a dedicated OPC Gateway, or an HMI model with a specialized AC 800M driver.

Q2: Do I need to reprogram the AC 800M controller when replacing the PP835A?
No. The core control program remains untouched. You only need to map the new HMI tags to the process variables already published by the controller or OPC Server.

Q3: What causes write failure when controlling pumps or valves from a new HMI?
Write failures usually result from incorrect DCOM security settings in OPC DA, misconfigured user permissions in OPC UA, or tag data type mismatches between the HMI and the OPC Server.

Guide to ABB CI857K01 INSUM Interface and Hot Swap Support

Guide to ABB CI857K01 INSUM Interface and Hot Swap Support

Optimizing Motor Control with the ABB CI857K01 Communication Interface Module

The Strategic Value of INSUM Integration in Industrial Automation

The ABB CI857K01 acts as a vital bridge between the AC 800M control system and intelligent motor control devices. By utilizing the INSUM (Integrated System for User-optimized Motor control) protocol, this module enables seamless data exchange. Modern process industries like oil, gas, and power generation rely on this real-time connectivity. It shifts maintenance strategies from reactive fixes to predictive insights. Consequently, operators can monitor motor health directly from the DCS (Distributed Control System) interface.

Guide to ABB CI857K01 INSUM Interface and Hot Swap Support

Technical Insights into Hot Swap Capabilities

The CI857K01 supports “Hot Swap” functionality under specific system architectures. When engineers install it within an S800 I/O station featuring redundant power, they can replace the module online. However, a brief communication interruption occurs during the physical swap. Therefore, it is not a “bumpless” transition for the data link. Engineers must ensure that connected drives enter a safe “last-state” or local mode during the replacement process. This prevents unexpected process trips in continuous manufacturing environments.

Advanced Communication and Predictive Diagnostics

Unlike standard digital I/O, the CI857K01 retrieves deep diagnostic data. It captures thermal status, trip history, and precise overload levels. This granular information reduces troubleshooting time for field technicians significantly. As a result, users can identify specific faults within the Motor Control Center (MCC) remotely. Moreover, centralized data acquisition helps plant managers optimize energy consumption across high-power motor fleets.

Electrical Robustness and Environmental Resilience

Industrial environments often face significant electromagnetic interference (EMI) from Variable Frequency Drives (VFDs). The CI857K01 meets stringent industrial-grade EMC standards to maintain signal integrity. In addition, its design handles temperature fluctuations common in heavy industrial cabinets. Nevertheless, field experience shows that improper grounding remains a leading cause of bus errors. Technicians should always ground the cable shield at one end to prevent disruptive ground loops.

Installation and Maintenance Best Practices

To ensure long-term reliability of the communication interface, follow these technical protocols:

  • ✅ Use high-quality shielded twisted-pair cables specifically rated for INSUM bus speeds.
  • ✅ Verify node addressing during commissioning to prevent duplicated ID conflicts.
  • ✅ Secure modules firmly on the DIN rail to withstand vibrations in mining or offshore applications.
  • ✅ Periodically inspect terminal tightness to avoid intermittent connection failures.

Selection Differences and Compatibility Standards

Choosing the right module requires understanding the distinction between the CI857K01 and other ABB interfaces like the CI854 (Profibus) or CI853 (RS-232). The CI857K01 is purpose-built for the INSUM ecosystem. While it integrates perfectly with AC 800M controllers, older legacy systems may require firmware upgrades. In addition, always check the compatibility of your Control Builder engineering tool version before finalizing the hardware selection.

Expert Commentary from Powergear X Automation Limited

At Powergear X Automation Limited, we believe the CI857K01 represents a shift toward more “intelligent” hardware layers. While many generic gateways exist, the native integration provided by ABB ensures higher data throughput and better reliability. However, users should not overlook the “human element.” Proper training in interpreting INSUM diagnostics is essential to realize the full ROI of this technology. We recommend this module for any facility aiming for Tier 1 digitalization in their motor control infrastructure.

Industrial Application Scenarios

  • Chemical Processing: Monitoring pump motors to prevent leaks or overheating in hazardous zones.
  • Power Generation: Synchronizing cooling fan motors with main boiler control loops.
  • Water Treatment: Centralized management of large-scale filtration and pumping stations.

Frequently Asked Questions (FAQ)

Q: Does the CI857K01 support redundant communication links?
The module itself is a single interface, but the AC 800M system supports redundant module configurations. By installing two CI857K01 modules in a redundant I/O base, you can achieve high-availability communication for mission-critical motor control loops.

Q: What is the most common mistake during INSUM commissioning?
In our experience, duplicated node IDs and improper bus termination are the most frequent issues. If the end-of-line resistor is missing, the signal reflections will cause sporadic communication dropouts that are difficult to diagnose.

Q: Can I use the CI857K01 to control non-ABB drives?
The CI857K01 is optimized for the ABB INSUM protocol. While some third-party devices claim compatibility, it is often better to use a standard Profibus (CI854) or Modbus (CI867) module for multi-vendor hardware environments to ensure full feature support.

For more information on high-quality ABB components and professional automation solutions, please visit the official Powergear X Automation Limited website.

ABB DCS Communication: Why CI873A Beats CI858 for Mixed Drives

ABB DCS Communication: Why CI873A Beats CI858 for Mixed Drives

CI873A vs CI858: Achieving Stability with Third-Party VFDs in ABB DCS

The Integration Challenge in Modern Industrial Automation

Integrating third-party variable frequency drives (VFDs) into an ABB DCS environment requires careful protocol selection. While hardware quality matters, communication stability often depends on the underlying network architecture. Many engineers face a choice between the CI873A and the CI858 modules. At Powergear X Automation, we observe that the CI873A typically offers superior reliability for non-ABB drives. This stability stems from its use of the globally recognized PROFIBUS DP standard rather than proprietary interfaces.

ABB DCS Communication: Why CI873A Beats CI858 for Mixed Drives

Protocol Architecture: PROFIBUS DP vs. DriveBus

The fundamental difference between these two modules lies in their communication language. The CI873A functions as a PROFIBUS DP master interface. This open standard is the native tongue for manufacturers like Siemens, Danfoss, and Schneider. Conversely, the CI858 utilizes DriveBus, a protocol specifically optimized for the ABB drive ecosystem. Using CI873A allows you to import GSD files directly into the DCS. As a result, you eliminate the need for complex protocol conversion gateways that often introduce latency.

Ensuring Deterministic Performance in Factory Automation

The CI873A provides highly deterministic polling, which is essential for precise motor control. In most production environments, PROFIBUS DP maintains a bus cycle time between 5ms and 20ms. This consistency ensures that speed references and alarm feedback remain synchronized with the process. In addition, third-party drives rarely support the full feature set of DriveBus. Therefore, opting for the CI873A prevents unpredictable communication behavior in mixed-vendor hardware lineups.

Diagnostic Transparency and Rapid Troubleshooting

Standardized diagnostics give the CI873A a significant edge for maintenance teams. It provides clear visibility into bus faults, node status, and device-specific telegrams. When a drive goes offline, engineers can immediately distinguish between a cable fault and a hardware failure. This transparency is critical in large-scale plants with dozens of nodes. Moreover, Powergear X Automation experts suggest that standard PROFIBUS tools simplify the validation of signal integrity during commissioning.

Field-Proven Best Practices for PROFIBUS Stability

Physical installation quality often dictates the long-term success of your communication network. Many intermittent faults trace back to improper shielding or termination. To ensure a robust system, we recommend following these technical guidelines:

  • ✅ Enable termination only at the physical ends of the bus.
  • ✅ Use active PROFIBUS connectors for segments with high node counts.
  • ✅ Implement metal-locking connectors in high-vibration pump rooms.
  • ✅ Verify that GSD file versions match the drive firmware exactly.
  • ✅ Maintain separate grounding points to avoid electrical noise interference.
  • ✅ Route communication cables away from high-voltage power lines.

Strategic Procurement: Making the Right Selection

Choosing the right module depends on your long-term plant strategy. The CI858 remains an excellent choice for purely ABB-driven environments. However, the CI873A is the safer investment for facilities using multiple drive brands. It reduces integration complexity and lowers the risk of vendor lock-in. Before purchasing, always confirm your AC 800M controller firmware version and node license limits. Proper planning ensures a smooth migration and reliable deterministic execution for your control system.

Industrial Solution Scenarios

  • Water Treatment: Integrating various pump drives via a single PROFIBUS backbone.
  • Chemical Processing: Maintaining stable speed control for mixers across different vendors.
  • Conveyor Systems: Utilizing standardized diagnostics to minimize downtime in logistics hubs.

Frequently Asked Questions (FAQ)

Q1: Can I mix ABB and non-ABB drives on the same CI873A bus?

Yes, PROFIBUS DP supports multi-vendor environments perfectly. You simply need the correct GSD file for each specific drive model. Ensure the total bus load remains within the CI873A technical limits for optimal performance.

Q2: Why is my third-party drive failing to initialize on the bus?

This is frequently caused by a mismatch in the Process Data Object (PPO) type. Check that the data length configured in the DCS matches the drive’s internal mapping. Also, verify that the PROFIBUS address on the drive hardware matches the software configuration.

Q3: How many drives can a single CI873A module support effectively?

While the protocol supports up to 125 nodes, practical engineering limits are usually lower. For high-performance motor control, we recommend staying below 32 nodes per segment. This ensures faster cycle times and easier segment isolation during maintenance.

Explore our full range of industrial communication modules at Powergear X Automation to find the perfect fit for your next DCS project.

Understanding CI871K01 PROFINET IO Support for AC 800M DCS

Understanding CI871K01 PROFINET IO Support for AC 800M DCS

Evaluating ABB CI871K01 PROFINET Version Support and System Impact

Defining the Role of CI871K01 in Modern DCS

The ABB CI871K01 (3BSE056767R1) serves as a dedicated PROFINET IO interface for the AC 800M controller family. It enables seamless communication between the DCS and decentralized field devices like drives and remote I/O. In industrial automation, this module bridges the gap between high-level control and Ethernet-based field networks. Many facilities use the CI871K01 when transitioning from traditional PROFIBUS to modern industrial Ethernet architectures. Consequently, it remains a staple in chemical processing, power generation, and large-scale manufacturing sectors.

Understanding CI871K01 PROFINET IO Support for AC 800M DCS

Technical Realities of PROFINET V2.2 Specification

The CI871K01 strictly adheres to the PROFINET V2.2 specification rather than the newer V2.3 version. This distinction significantly influences system design and device selection. V2.2 primarily supports Real-Time (RT) Class 1 communication, which provides deterministic performance for most process tasks. However, it does not support Isochronous Real-Time (IRT) functions required for high-speed motion control. At Powergear X Automation, we suggest verifying your cycle time requirements before deployment. Standard RT communication typically offers stable 4ms to 10ms update rates.

Optimizing Ethernet Performance for Factory Automation

This module utilizes 10/100 Mbps Fast Ethernet to manage hundreds of cyclic I/O signals efficiently. High bandwidth ensures that the network remains stable even in complex distributed I/O topologies. Moreover, the CI871K01 maintains deterministic communication to prevent bus saturation in busy production environments. In typical packaging or refinery setups, one module easily handles dozens of PROFINET devices. Therefore, engineers can expand their field networks without compromising the integrity of the control system.

Streamlining Integration with Control Builder M

The CI871K01 integrates directly with the AC 800M platform via the Control Builder M engineering tool. This deep integration allows for automatic device parameterization using standard GSDML files. Furthermore, it centralizes hardware diagnostics within the System 800xA environment for easier troubleshooting. This approach reduces manual configuration errors and shortens commissioning timelines significantly. As a result, maintenance teams can identify field faults quickly without needing third-party diagnostic software.

Crucial Field Insights from Powergear X Automation

Our team at Powergear X Automation often observes GSDML version conflicts during site upgrades. Since the CI871K01 supports V2.2, newer devices may require backward-compatible configuration files. In addition, physical installation quality determines long-term reliability in high-vibration areas like turbine halls. Always ensure the module locks securely onto the TP867 baseplate to prevent intermittent communication alarms. We recommend using managed industrial switches and VLAN segmentation to protect the PROFINET traffic from broadcast storms.

Hardware Maintenance and Reliability Tips

  • ✅ Confirm device GSDML compatibility with PROFINET V2.2 standards.
  • ✅ Utilize managed switches to monitor network health effectively.
  • ✅ Inspect CEX-bus connectors during every scheduled plant shutdown.
  • ✅ Apply VLAN tagging to isolate control traffic from office data.
  • ✅ Secure all module locking mechanisms in high-vibration environments.
  • ✅ Verify IP address assignments to avoid network identity conflicts.

Industrial Solution Scenarios

  • Hybrid Migrations: Integrating PROFINET remote I/O into existing PROFIBUS-heavy AC 800M systems.
  • Drive Integration: Controlling multiple frequency converters in a water treatment facility.
  • Legacy Support: Replacing failed units in 800xA systems commissioned between 2008 and 2016.

Strategic Procurement FAQ

Q1: Should I choose the CI871K01 or the newer CI871A for new projects?

For new installations, we recommend the CI871A or CI871AK01. These newer versions support PROFINET V2.3 and offer better compatibility with modern intelligent devices. The CI871K01 is best suited as a direct spare part for existing legacy systems.

Q2: Can this module support redundant PROFINET configurations?

The CI871K01 lacks native support for System Redundancy (SR) or Media Redundancy Protocol (MRP) at the module level. You must implement network resilience at the switch level. For high-availability requirements, consult the latest ABB hardware compatibility lists for redundant interface options.

Q3: What happens if I use a V2.3 GSDML file with this module?

Using an incompatible GSDML file often leads to configuration errors in Control Builder M. The software may fail to recognize specific device parameters or diagnostic blocks. Always request the V2.2 compatible GSDML version from your hardware vendor to ensure full functionality.

Back to Top
Product has been added to your cart