Over 50,000 hot-selling automation module components.

Fix TM218LDA40DR2HN STAT LED Yellow Green Flashing | M218 PLC

Troubleshooting Schneider M218 TM218LDA40DR2HN STAT LED Flashing Yellow and Green

Front-panel LED status indicators on Schneider Electric Modicon M218 controllers offer fast operational diagnostics for automation engineers. The TM218LDA40DR2HN controller displays alternating yellow and green on its STAT LED during system startup. This signal indicates the CPU is currently booting or running self-diagnostic checks. Powergear X Automation provides this troubleshooting guide to help technicians diagnose initialization stalls and restore reliable control system performance.
Understanding CPU Status States in Industrial Automation Systems

The STAT LED reflects the active lifecycle phase of the Modicon M218 PLC. Solid green confirms normal RUNNING mode, while flashing green indicates a STOPPED state. Alternating yellow and green signals system initialization immediately following power-up. However, a controller stuck in this startup phase prevents the system from entering its automated cycle. Engineers must recognize that initialization stalls stem from power quality or hardware configuration issues rather than immediate CPU failure.

Power Supply Quality and Voltage Drop Factors in Factory Automation

Unstable 24VDC control power frequently disrupts the boot sequence of programmable logic controllers. Heavy inductive loads like contactors and solenoid valves generate severe voltage drops when wired to the same power supply. Moreover, aging power supplies introduce excessive ripple voltage into the main processor. As a result, the controller repeatedly reboots or fails to complete initialization. Isolating PLC power with a dedicated power supply ensures clean startup voltage.

Firmware Compatibility and Machine Expert Programming Standards

Firmware mismatches between the controller hardware and the programming environment cause severe initialization delays. Upgrading CPU units without verifying firmware compatibility stops the boot routine. In addition, missing TM2 or TM3 expansion I/O modules cause hardware handshake errors during startup. Engineers must review application project files in EcoStruxure Machine Expert before replacing active controllers in operational production lines.

Step-by-Step Commissioning and Diagnostic Sequence for M218 PLCs

  1. Monitor Startup Duration: Observe the STAT LED during power-up to confirm if it resolves to green within thirty seconds.
  2. Inspect 24VDC Power Terminal Voltage: Measure input voltage at the PLC terminals during load changes to verify voltage stability.
  3. Connect Machine Expert Diagnostics: Link the controller via USB or Ethernet to read internal system fault logs and diagnostic messages.
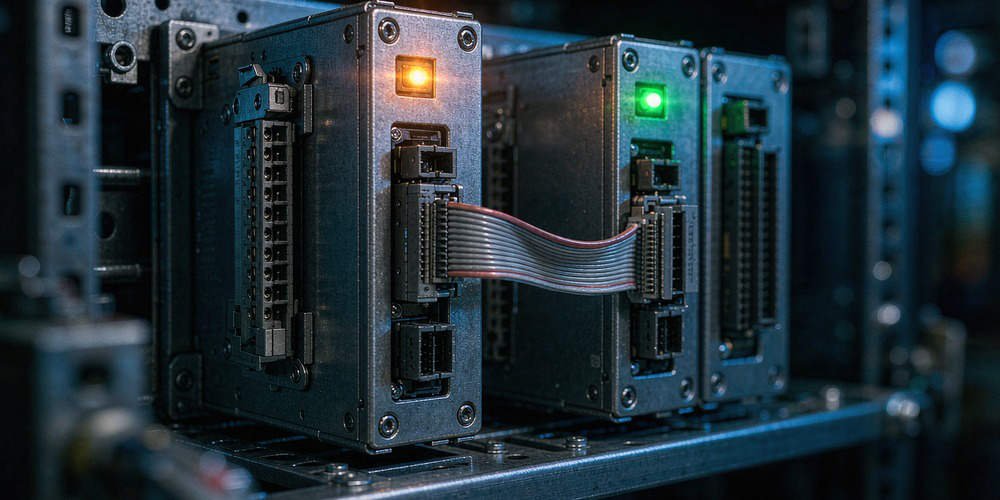
  4. Verify Expansion Module Bus Connections: Inspect physical ribbon cables on TM2 and TM3 modules for loose connections or misconfigurations.

Field Installation Practices and Noise Suppression Standards

High electromagnetic interference in motor control cabinets triggers frequent CPU resets and bus communications errors. Signal wiring running parallel to variable frequency drive cables induces unwanted electrical noise. Therefore, control panel designs must follow international electrical safety standards such as IEC 60204-1. Installing shielded twisted-pair cables and proper single-point grounding protects delicate analog and digital circuits against noise corruption.

B2B Procurement Guidelines for Modicon M218 Spare Parts

Procurement teams should evaluate system compatibility prior to ordering replacement controllers. Replacing a damaged TM218LDA40DR2HN unit requires matching physical I/O specifications and software firmware revisions. In addition, purchasing verified legacy components reduces line shutdown risk during critical maintenance windows. Maintenance departments should store fully tested backup CPUs containing pre-loaded project configurations for rapid emergency replacement.

Application Scenario: Packaging Machine Initialization Recovery

A high-speed cartoning system unexpectedly stopped operating after a routine facility power outage. The installed TM218LDA40DR2HN controller displayed an alternating yellow and green STAT LED continuously for over ten minutes. The site technician initially assumed a failed PLC processor and requested an immediate hardware swap.

Upon site investigation, the engineering team discovered an unstable 24VDC power supply output dropping to 18VDC whenever downstream safety relays energized. The team installed a dedicated industrial 24VDC power supply exclusively for the PLC and added surge suppressors across all solenoid coils. Upon rebooting, the STAT LED transitioned from yellow-green to solid green within eight seconds, restoring full machine operation without needing a replacement controller.

To source genuine Schneider Electric PLC hardware and access reliable industrial components, visit Powergear X Automation to explore complete factory automation solutions.

Frequently Asked Questions (FAQ)

Q1: Does a yellow and green flashing STAT LED indicate a permanently damaged CPU?
No. This pattern normally indicates routine system booting and hardware initialization. It only signals a hardware defect if the state persists indefinitely despite stable power and valid firmware.

Q2: How long should the STAT LED flash yellow and green during a normal startup?
Under normal operating conditions, the STAT LED transitions to solid green or flashing green within five to thirty seconds, depending on application size and connected expansion modules.

Q3: Can I swap a TM218LDA40DR2HN controller without updating Machine Expert project files?
You can swap units directly only if the replacement unit shares the exact same firmware revision and memory configuration. Mismatched firmware versions require project recompilation and re-downloading.
Fix Honeywell CC-PAOH01 0 mA Error and Phantom Voltage Faults

Troubleshooting Honeywell CC-PAOH01 Analog Output 0 mA Error and Voltage Residuals

In modern industrial automation systems, precision control of process variables relies heavily on reliable DCS I/O modules. The Honeywell Experion PKS Series 8 CC-PAOH01 analog output card converts controller directives into 4-20 mA current loops. These loops drive control valve positioners, variable speed drives, and field actuators. However, engineers frequently encounter a puzzling symptom where output terminals display voltage while loop current reads 0 mA. Powergear X Automation provides this troubleshooting guide to resolve this issue without prematurely condemning internal fuses.

Core Value of Precision Analog Output Modules in Process Control

The CC-PAOH01 module delivers precise analog control signals to ensure stable process regulation across petrochemical and pharmaceutical facilities. According to recent industrial automation reliability reports, over 35% of unscheduled control loop downtime stems from field wiring issues rather than internal PLC card failures. Accurately diagnosing whether a 0 mA failure originates from field wiring or internal circuitry prevents unnecessary card replacements. Consequently, proper diagnostic procedures significantly reduce plant downtime and maintenance expenditures.

Technical Insights: Open-Circuit Voltage versus Current Loop Integrity

The Honeywell CC-PAOH01 features 16 HART-enabled HART analog output channels supporting load resistances up to 800 ohms under standard 24 VDC power. Field technicians must understand that terminal voltage does not guarantee current flow. High-impedance digital multimeters often register phantom voltage induced by floating circuit potential or nearby cable coupling. If a field wire breaks or a terminal block connection looses, current drops to zero immediately. Therefore, measuring terminal voltage alone offers incomplete diagnostic information.

Analyzing Loop Load Resistance and Overload Circuit Protection

The module operates within a strict supply range of 22 to 28 VDC across long-distance cable runs. Excessive loop resistance from added isolators or safety barriers prevents the module from driving the target current. Conversely, severe short circuits trigger internal overcurrent protection mechanisms to safeguard internal components. Industry experts at Powergear X Automation observe that Honeywell Series-C I/O modules integrate short-circuit protection, minimizing the reliance on traditional internal glass fuses. Thus, external terminal assemblies usually house any physical fuses present.

Deciphering Channel Diagnostics, HART Data, and Safety States

Honeywell Experion PKS software provides comprehensive channel-level diagnostics, including open-circuit detection and output deviation alarms. When electronic faults occur, the CC-PAOH01 automatically defaults to a configured fail-safe 0 mA state. Engineers must check whether the DCS controller actually demands a 0 mA output before troubleshooting hardware. Moreover, HART diagnostic data from field instruments helps verify whether the actuator electronics remain healthy. Always obtain operational permits before modifying channel fail-safe options or testing critical control valve loops.

Step-by-Step Diagnostic Sequence for 0 mA Loop Failures

  1. Check Controller Output Command: Verify in Experion PKS that the channel command value exceeds 0 mA and check active alarm logs.
  2. Inspect Field Wiring Integrity: Test cable continuity, barrier connections, and terminal block tightness using appropriate schematic diagrams.
  3. Measure True Loop Current: Connect a calibrated multimeter in series with the loop rather than placing voltage probes directly across terminals.
  4. Validate IOTA Power and Module Status: Inspect power input on the Input Output Termination Assembly (IOTA) and check channel readback values.

Differentiating Internal Module Protection from External Fuse Failures

Misinterpreting external protection trips as internal module failures leads to costly inventory errors. Honeywell Series-C architectures feature electronic short-circuit suppression on both input and output circuits. However, specialized Universal Marshalling Field Termination Assemblies (FTA) may incorporate external M5 x 20 mm glass fuses. Technicians should isolate power and check external fuse continuity when terminal voltage appears floating. Replacing a blown external fuse resolves the 0 mA condition without replacing the CC-PAOH01 card.

Compatibility Guidelines for Module Replacement and Procurement

Procurement teams must carefully verify hardware revisions when sourcing replacement DCS components. The CC-PAOH01 module supports HART communication and cannot directly swap with non-HART variants like the CC-PAOX01 or CC-PAON01. Furthermore, system integrators must match the module with appropriate IOTA bases, such as the CC-TAOX01 non-redundant or CC-TAOX11 redundant models. Verify Experion PKS software compatibility and hardware revision levels prior to scheduling maintenance downtime.

Application Scenario: Chemical Plant Control Valve Diagnostics

A chemical processing plant experienced a sudden failure when a critical feed valve closed unexpectedly. The DCS operator console indicated a 4 mA demand, but the field valve positioner received 0 mA. A field technician measured 21.5 VDC across the terminal block and initially declared the CC-PAOH01 card defective.

Powergear X Automation engineers recommended a systematic continuity check before swapping the module. The maintenance crew discovered a corroded marshalling panel terminal that created an open circuit under load. Repairing the physical connection immediately restored the 4-20 mA current loop and re-established automatic valve control without replacing the CC-PAOH01 module.

To source genuine Honeywell DCS parts and explore robust control solutions, visit Powergear X Automation for technical expertise and reliable equipment delivery.

Frequently Asked Questions (FAQ)

Q1: Why do I measure voltage across the CC-PAOH01 terminals when current is 0 mA?
Voltage presence with zero current typically indicates an open loop, such as a broken wire, loose terminal, or blown external fuse. High-impedance multimeters can also display phantom voltage from internal drive circuits when no load completes the circuit.

Q2: Does the CC-PAOH01 module contain internal field-replaceable fuses?
No. Honeywell Series-C CC-PAOH01 modules utilize solid-state electronic short-circuit protection. Fuses are typically located on external Field Termination Assemblies (FTA) or specialized marshalling terminal blocks.

Q3: Can I replace a CC-PAOH01 module with a CC-PAOX01 card?
No. The CC-PAOH01 supports HART digital communications, whereas the CC-PAOX01 does not. Swapping these cards causes configuration errors in Experion PKS and disrupts HART field device diagnostics.

Fix IC695CPE400 Non-Safety Faults & System Shutdown Errors

Why Non-Safety Faults Cause Total System Shutdowns in PACSystems RX3i IC695CPE400 Control Systems

Modern process plants rely heavily on high-performance controllers for distributed control systems (DCS) and factory automation. The Emerson PACSystems RX3i IC695CPE400 standalone controller delivers impressive processing power for demanding applications. However, control engineers often ask why non-safety domain errors trigger complete plant shutdowns. Powergear X Automation presents this technical analysis to clarify the structural limits of multi-core processors, error propagation mechanisms, and functional safety isolation in modern PLCs.

Multi-Core Processors versus Physical Safety Isolation in Factory Automation

The IC695CPE400 controller features a quad-core AMD G-Series processor running a real-time VxWorks operating system. System integrators often assume that multi-core architectures provide true physical isolation between standard control and safety tasks. However, task separation on shared silicon does not equal certified functional safety isolation. A software-based safety task inside a standard PLC cannot achieve Safety Integrity Level (SIL) ratings. Therefore, critical safety functions must always run on dedicated, independently certified safety controllers.

Root Causes of Non-Safety Errors Triggering Global Controller Shutdowns

A non-safety fault can halt the entire PACSystems RX3i controller due to shared hardware resources. Heavy Ethernet traffic from SCADA or OPC UA clients can exhaust controller memory queues. Consequently, communication overload delays real-time control task execution and triggers the internal hardware watchdog timer. Furthermore, uncorrectable multi-bit ECC memory errors or bus faults force the CPU into a fatal STOP HALT state. As a result, the controller revokes all output scanning regardless of logic task prioritization.

Evaluating Output Behaviors and Final Element States During PLC Halt Events

When an IC695CPE400 controller enters a STOP state, field actuators behave according to hardware configurations and circuit designs. Industrial safety standards like IEC 61511 and IEC 60204-1 require predictable fail-safe states during control failure. However, holding last state on digital outputs can create severe process hazards during unexpected shutdowns. Engineers must design independent hardwired trip circuits to ensure critical valves close safely even when the main CPU halts.

Systematic Troubleshooting Steps for Controller Faults and Shutdown Events

  1. Check Controller Status LEDs: Inspect the PWR, FLT, and OE indicators on the front panel to identify CPU fault states.
  2. Extract PLC Fault Tables: Connect PAC Machine Edition software to capture error logs and time stamps before clearing memory.
  3. Trace Error Propagation Paths: Compare network traffic spike times with CPU watchdog timeout events to isolate the root cause.
  4. Verify Safety Circuit Integrity: Test independent trip relays to ensure safety interlocks operate without CPU intervention.

Field Installation and Network Segmentation Best Practices

Isolating critical control networks from enterprise IT systems prevents external communication faults from affecting PLC performance. Engineers should deploy industrial firewalls and strict access control rules to limit unrestricted polling. Moreover, field technicians must avoid unthrottled Modbus TCP requests within fast ladder logic loops. Proper network architecture protects controller resources, minimizes processor load, and improves overall system stability across automated facilities.

B2B Hardware Procurement and Firmware Compatibility Guidelines

Replacing an IC695CPE400 controller requires thorough compatibility verification before scheduling plant maintenance. Procurement managers must verify hardware revision numbers, backplane firmware versions, and PAC Machine Edition software compatibility. Deploying unmatched firmware releases can lead to unexpected watchdog resets and diagnostic alarm losses. Therefore, engineering teams should conduct offline configuration tests before installing new hardware on live production lines.

Application Scenario: Chemical Reactor Emergency Shutdown Protection

A continuous chemical processing plant experienced repeated reactor shutdowns caused by high OPC UA polling rates on an IC695CPE400 controller. The excessive network traffic saturated processor buffers, causing a watchdog timeout that halted all digital output modules. Consequently, the main feed pumps stopped abruptly, disrupting plant production for several hours.

To resolve the issue, the engineering team separated the SCADA data collection network using an industrial managed switch with rate limiting. Furthermore, they transferred the emergency reactor trip logic to an independent SIL-certified safety relay system. This architecture prevented network traffic spikes from halting the CPU while ensuring absolute safety protection for critical reactor valves.

To source original Emerson PACSystems RX3i hardware and receive expert engineering support for your DCS infrastructure, visit Powergear X Automation to explore reliable control system solutions.

Frequently Asked Questions (FAQ)

Q1: Does the IC695CPE400 multi-core processor eliminate the need for a separate safety PLC?
No. Multi-core execution inside a standard controller does not satisfy IEC 61511 functional safety standards. Certified safety PLCs require physical redundant architectures, diagnostic coverage, and hardware fault tolerance that standard PLCs lack.

Q2: Should I immediately replace the IC695CPE400 CPU if the FLT LED turns red?
Not necessarily. A red FLT light indicates a fatal fault, which often stems from software logic errors, network buffer overflows, or firmware mismatches rather than permanent hardware failure. Always check the PLC Fault Table first.

Q3: How does network segmentation improve PACSystems RX3i controller reliability?
Network segmentation isolates real-time I/O traffic from high-volume enterprise data requests. Limiting non-critical network traffic prevents communication buffer exhaustion and reduces the risk of CPU watchdog timeouts.

Honeywell CC-PUIO01 220V AC Damage & Module Failure Analysis

Honeywell CC-PUIO01 Channel Breakdown and Module Failure Analysis After Accidental 220V AC Overvoltage

In modern DCS and factory automation systems, universal input output modules offer extreme flexibility. However, field technicians often encounter severe overvoltage damage during maintenance or wiring upgrades. Connecting 220V AC mains voltage to low-voltage I/O terminals instantly destroys delicate electronic components. Powergear X Automation presents this technical analysis to explain how single-channel voltage spikes cascade into module-wide failures within Honeywell Experion PKS Series C platforms.

Multi-Signal Flexibility and Integrated Architecture in Industrial Control Systems

The Honeywell CC-PUIO01 module handles analog inputs, analog outputs, digital inputs, and digital outputs on a single card. Industrial facilities utilize these universal channels to streamline hardware configurations across process control networks. However, this high level of integration creates shared power rails and internal circuitry. Consequently, wiring errors quickly propagate beyond the initial point of contact, jeopardizing adjacent I/O loops and plant safety.

Technical Analysis of Channel Breakdown and Shared Circuit Failure

Universal channels operate within strict low-voltage thresholds, typically supporting 0-20mA or 4-20mA current loops. Applying 220V AC directly to signal terminals exceeds semiconductor breakdown voltages immediately. Furthermore, semiconductor protection diodes fail under continuous AC current stress. As a result, high voltage surges bypass channel isolation, destroying internal power converters and backplane communication microcontrollers.

Differentiating Electronic Short-Circuit Protection from AC Overvoltage Protection

Engineers must not confuse output short-circuit protection with AC mains voltage tolerance. Honeywell builds short-circuit protection to handle current overloads within DC voltage limits. However, 220V AC mains power delivers destructive energy that melts printed circuit board traces. Moreover, latent thermal stress degrades surrounding components, causing unpredictable drift or sudden failures weeks after the initial incident.

Step-by-Step Field Recovery and Troubleshooting Protocol

  1. Isolate System Power Immediately: De-energize all field wiring and disconnect the main power supply before inspecting damaged cabinets.
  2. Perform Visual and Physical Audits: Inspect terminal blocks, I/O Termination Assemblies (IOTA), and PCB traces for discoloration or burnt components.
  3. Conduct Offline Multi-Channel Testing: Benchmark loop accuracy on unexposed channels using calibrated signal injectors before reconnecting field devices.
  4. Review Diagnostic Logs in Experion PKS: Analyze system event journals to verify backplane communication health and internal power diagnostic flags.

Establishing Robust Field Wiring Safety Standards

Preventing high-voltage cross-connections requires strict physical isolation standards across control cabinets. Engineers must segregate 220V AC power distribution lines from 24V DC instrument cables inside dedicated wire ducts. Additionally, clear color-coded terminal blocks and voltage labels reduce human error during night-shift maintenance. Implementing interposing isolation relays provides an additional hardware barrier for field signals entering sensitive PLC or DCS modules.

Strategic Procurement Guidelines for Series C Replacement Hardware

Replacing damaged CC-PUIO01 modules requires verifying hardware revisions and firmware compatibility. Procurement managers should cross-reference part numbers, IOTA base requirements, and Experion PKS software release notes. Furthermore, installing pre-tested, certified spare parts minimizes unexpected shutdown risks during plant re-commissioning. Always source replacement modules from reliable industrial suppliers to ensure long-term operational stability.

Application Scenario: Petrochemical Distillation Column Overvoltage Incident

During a turnaround maintenance event at a refinery, a contractor accidentally landed a 220V AC solenoid power cable onto a 4-20mA pressure transmitter input terminal connected to a CC-PUIO01 module. The overvoltage destroyed the primary channel instantly and tripped the internal DC-DC converter, causing five adjacent flow control loops to drop offline.

The plant engineering team isolated the field power and removed the damaged module. They replaced the burnt I/O card with a certified unit and verified signal calibration across all sixteen channels. By enforcing strict wire-tagging rules and conducting full loop validation before startup, the facility restored production safely within four hours, preventing extended unit downtime.

To acquire high-quality DCS hardware and expert technical support for Honeywell Series C systems, visit Powergear X Automation to explore our extensive automation inventory.

Frequently Asked Questions (FAQ)

Q1: Can I still use the remaining channels on a CC-PUIO01 module if only one channel burned out from 220V AC?
No. Overvoltage surges often degrade shared internal power circuits and silicon insulation. Operating a partially damaged module risks unpredictable signal drift, intermittent communication drops, or complete module failure during critical operations.

Q2: Does the Honeywell CC-PUIO01 module feature built-in protection against 220V AC miswiring?
No. The module features short-circuit and overcurrent protection for low-voltage DC signals. High-voltage AC electricity exceeds internal component limits and destroys input conditioning circuits instantly.

Q3: What steps are necessary before inserting a replacement CC-PUIO01 module into an active Experion PKS system?
First, rectify the field wiring fault and verify voltage levels with a multimeter. Second, inspect the IOTA base for physical damage. Finally, seat the new module and load the configuration via Experion PKS software.

Honeywell FC-RUSIO Flashing Yellow STBY Diagnostics Guide

Decoding Honeywell FC-RUSIO Yellow Flashing STBY Status in Safety Systems

In high-stakes industrial automation, reliable safety instrumented systems protect critical manufacturing assets. The Honeywell FC-RUSIO Universal Safety I/O module handles field inputs for Safety Manager and Experion PKS DCS architectures. However, engineers frequently encounter a yellow flashing STBY indicator during module initialization or switchover. Powergear X Automation provides this practical diagnostic guide to help technicians interpret intermediate standby states correctly without risking safety trips.

Understanding Standby States in Redundant Control Systems

The STBY indicator signals the secondary module status within a redundant safety pair. According to ISA-84 safety standards, redundant hardware must verify memory synchronization before taking active control. A yellow flashing light usually indicates an intermediate state, such as boot-up or database qualification. Therefore, operators must not assume the secondary module is fully ready for automatic failover during this phase.

Evaluating Root Causes of Intermediate Yellow Flashing Statuses

Several factors cause the STBY LED to flash yellow on FC-RUSIO modules during operation. Modern factory automation environments demand strict hardware and firmware alignment between redundant pairs. An ongoing synchronization process or mismatched firmware version holds the module in a qualification loop. Moreover, minor communication faults across the redundant backplane prevent the standby unit from reaching fully synced status.

Ensuring Safety Integrity During Module Maintenance and Swaps

Safety System Integrity Level compliance requires strict verification before executing hot swaps. Field technicians must never rely solely on front panel LED indicators. Instead, operators should check the Experion PKS system diagnostics to confirm database consistency. In addition, technicians must review active bypasses and safety interlocks prior to cycling power on redundant I/O cards.

Step-by-Step Diagnostic Sequence for Honeywell I/O Troubleshooting

  1. Record All Module LEDs: Document the status of the FAULT, RUN, and STBY indicators simultaneously.
  2. Check System Diagnostics: Access the Safety Manager software to view detailed event logs and error codes.
  3. Verify Firmware Consistency: Confirm that the primary and secondary FC-RUSIO modules share identical firmware revisions.
  4. Inspect Backplane Connections: Ensure proper seating and clean physical connections along the rack backplane.

Best Practices for Maintenance and Safety System Readiness

Unplanned shutdowns often occur when technicians force failovers on unready standby modules. According to ARC Advisory Group reports, improper maintenance procedures cause nearly 20% of industrial unscheduled downtime. Therefore, maintenance teams must maintain verified software backups and update system documentation regularly. Always follow approved plant safety procedures before manipulating live SIS hardware.

B2B Procurement and Compatibility Insights for Honeywell Parts

Procurement teams must carefully verify exact part numbers when ordering replacement safety modules. For example, buying an FC-RUSIO-3224 module requires verifying backplane compatibility and terminal assembly revisions. Installing mismatched hardware revisions can delay synchronization and disrupt DCS communications. Powergear X Automation recommends consulting certified automation specialists to ensure seamless module integration.

Application Scenario: Refined Chemical Plant SIS Maintenance

A petrochemical processing facility experienced a persistent yellow flashing STBY light after replacing a secondary FC-RUSIO module. The engineering team initially suspected a defective replacement card. However, diagnostic software logs revealed that the primary module ran firmware version 2.1, while the new module contained version 2.4.

The technical team aligned the module firmware using Safety Manager software tools. Once the firmware versions matched, the STBY LED transitioned from flashing yellow to solid yellow within 45 seconds. This process successfully re-established full redundant synchronization without interrupting plant production.

To source original Honeywell safety modules and access expert support for your control systems, visit Powergear X Automation to find high-performance components for your facility.

Frequently Asked Questions (FAQ)

Q1: Does a yellow flashing STBY light mean the FC-RUSIO module is faulty?
No. A yellow flashing light typically indicates an intermediate transition state, such as memory synchronization or firmware validation, rather than an active hardware failure.

Q2: Can I manually trigger a failover while the STBY light is flashing yellow?
No. Forcing a failover while the secondary module is unverified can drop field signals and trigger an unintended safety trip across your DCS.

Q3: Where can I confirm the exact LED definitions for my FC-RUSIO module revision?
Always consult the official Honeywell Safety Manager Hardware Guide or check Experion PKS system diagnostics for your specific firmware revision.

Honeywell FC-PSU-UNI2450U Smoke Diagnosis & Power Supply Guide

Honeywell FC-PSU-UNI2450U Smoke at Power-On: Diagnostic Guide for Power Supply Faults

A sudden emit of smoke from a Honeywell FC-PSU-UNI2450U power supply during post-overhaul energization demands immediate technical investigation. Industrial control systems rely on stable 24VDC power rails to maintain continuous safety manager operations. However, field engineers cannot immediately attribute power-on smoke solely to bridge rectifier breakdown or capacitor aging. Powergear X Automation provides this engineering assessment to isolate internal component failures, inrush current surges, and external wiring faults in process automation environments.

Understanding the Safety Manager Power Architecture

The FC-PSU-UNI2450U serves critical safety system components in DCS and PLC hardware environments. This module delivers regulated 25–28 VDC output specifically designed for high-reliability process safety applications. Unlike general-purpose industrial automation power units, safety manager power supplies integrate precise voltage monitoring and fast-acting protection logic. Therefore, engineers must avoid substituting this unit with standard commercial power supplies during facility maintenance or cabinet overhauls.

Analyzing Input Rectifier Failures and Inrush Current Impacts

Primary AC rectification components face severe thermal and electrical stress during initial system energization. An internal short circuit inside the bridge rectifier causes a massive AC input current surge upon power-on. Consequently, this sudden current draw trips input protection fuses, damages printed circuit boards, and generates visible smoke. However, metal oxide varistors, primary MOSFET switching devices, and input suppression circuits produce identical symptoms. Engineers must perform diode junction testing and resistance checks before declaring the rectifier as the root cause.

Evaluating Electrolytic Capacitor Aging and Dielectric Breakdown

DC bus electrolytic capacitors experience electrolyte drying, elevated Equivalent Series Resistance, and internal insulation degradation over time. High ESR typically causes excessive ripple voltage and thermal buildup during steady-state operation. However, severely aged capacitors can suffer dielectric breakdown during power-on inrush events. Visual indicators include bulging safety vents, electrolyte residue, and localized PCB discoloration. Furthermore, secondary collateral damage from a failed switching transistor can mimic direct capacitor failure, requiring thorough circuit tracing.

Technical Specifications and Thermal Operating Limits

Honeywell hardware reference manuals define strict operational parameters for the FC-PSU-UNI2450U power module. The unit guarantees a full-load hold-up time of 100 milliseconds to bridge momentary utility voltage dips. Moreover, operating ambient temperatures above 50°C trigger thermal derating profiles that shorten capacitor lifespan. Industrial plants must maintain cabinet ventilation to prevent heat accumulation, as excessive ambient temperatures accelerate insulation breakdown in both power semiconductor junctions and filter capacitors.

Step-by-Step Commissioning Isolation Protocol

  1. Secure System Isolation: Lock out the AC supply immediately and never re-energize a smoking power supply repeatedly.
  2. Verify Line Input Parameters: Measure incoming AC voltage, supply frequency, and mechanical connector retention clips for proper installation.
  3. Isolate Downstream Loads: Disconnect output terminals to differentiate between internal PSU short circuits and external load faults.
  4. Perform Component Resistance Tests: Check primary switching MOSFETs, rectifier diodes, and input MOVs with an multimeter prior to re-applying power.

Field Guidelines for Installation and Physical Maintenance

Proper mechanical assembly prevents premature power supply failures during plant commissioning. The FC-PSU-UNI2450U utilizes locking DC connectors and AC input retention clips to withstand cabinet vibration. Engineers must maintain vertical mounting orientations to facilitate natural convection cooling across the internal heat sinks. In addition, cleaning cabinet dust filters and verifying cooling fan operation significantly reduces thermal stress on high-voltage primary components.

B2B Procurement and Version Compatibility Review

Replacing legacy safety manager power supplies requires careful verification of hardware revisions and system catalog numbers. Honeywell documentation specifies FC-PSU-UNI2450U version 2.1 as a direct upgrade for older V1.0 and V2.0 models. However, legacy cabinet backplanes may require additional mechanical adapter plates or wiring harness updates. Purchasing teams should verify exact part numbers, revision levels, and firmware support with certified automation suppliers before executing plant upgrades.

Application Scenario: Petrochemical Refinery Commissioning

During a planned turnaround at a chemical processing facility, maintenance crews re-energized a safety instrumented system cabinet containing an FC-PSU-UNI2450U module. The power supply emitted smoke instantly, tripping the main cabinet circuit breaker. The plant engineering team isolated the supply and performed benchtop component analysis.

The diagnostic revealed that an line voltage transient had shorted the primary MOV surge suppressor, which subsequently damaged the adjacent bridge rectifier. The DC bus capacitors remained fully functional. The team replaced the damaged power module with a verified unit, inspected the AC input line filtering, and successfully restored safety system communications without further downtime.

For high-performance industrial control hardware, genuine safety system components, and expert technical support, visit Powergear X Automation to explore our comprehensive automation product portfolio.

Frequently Asked Questions (FAQ)

Q1: Can an external short circuit on the 24VDC output cause the power supply to smoke?
No, the FC-PSU-UNI2450U features built-in electronic short-circuit protection on its output stage. An external DC load fault causes output voltage collapse or hiccup mode protection, rather than immediate primary-side smoking.

Q2: How do I distinguish between a failed bridge rectifier and a shorted MOSFET?
Unplug the power supply and use a digital multimeter in diode-check mode. A shorted bridge rectifier shows zero resistance across the AC input pins or DC bus rails, whereas a shorted MOSFET displays low resistance specifically between its drain and source terminals.

Q3: Is the FC-PSU-UNI2450U directly interchangeable with Honeywell C300 power supplies?
No. While both systems use 24VDC power architectures, the FC-PSU-UNI2450U belongs to the Safety Manager family and possesses specific mechanical form factors, pinouts, and safety certification levels distinct from C300 series hardware.

ABB CI867 Modbus TCP Zero-Data Fix & Byte Swap Guide

Troubleshooting ABB CI867 Modbus TCP Zero-Data Faults and Byte Swap Issues After Module Replacement

Replacing an industrial communication interface in a distributed control system (DCS) often presents unexpected challenges. Maintenance teams frequently observe that replacing an ABB CI867 Modbus TCP module results in all field data displaying zero. However, the physical Link LED on the Ethernet port shows normal operation. Powergear X Automation provides this troubleshooting guide to resolve data integrity issues in ABB System 800xA and AC 800M control systems.

Distinguishing Physical Ethernet Connectivity from Modbus Application Integrity

A solid Link LED indicates a healthy physical Layer 1 Ethernet connection. However, physical layer stability does not guarantee correct application layer data exchange. Modbus TCP operates as a client-server protocol requiring precise register mapping and matching data formats. According to industrial networking surveys, over 40% of post-replacement field errors stem from software configuration mismatches rather than hardware defects. Therefore, engineers must separate physical connectivity from data interpretation when diagnosing all-zero readings.

Understanding Byte Swap and Word Swap Dynamics in Process Automation

Modbus TCP transmits 16-bit register pairs using standard big-endian byte ordering. However, multi-register 32-bit values like floating-point numbers require careful byte and word alignment. Swapping high and low bytes alters integer values within a single 16-bit word. Conversely, word swapping exchanges the positions of two adjacent 16-bit registers. While a byte swap mismatch generates incorrect numerical values, it rarely causes every register to read zero simultaneously.

Identifying Root Causes of All-Zero Readings in Factory Automation

When every Modbus register displays zero after module replacement, investigate underlying configuration mismatches. Common causes include incorrect starting register addresses, offset errors, and unsupported Modbus function codes. For instance, requesting Function Code 03 instead of Function Code 04 can cause quiet read failures. In addition, uninitialized application variables or missing communication status flags force PLC and DCS logic to output zero values for safety.

Step-by-Step Commissioning Sequence for CI867 Module Integration

  1. Verify Physical Communication: Confirm active IP configuration, subnet masks, and ping connectivity between the CI867 and remote devices.
  2. Capture Raw Register Data: Use Control Builder software or a Modbus poll utility to inspect unformatted hexadecimal register values.
  3. Validate Register Addressing: Verify whether the field instrument utilizes zero-based or one-based Modbus register addressing.
  4. Check Byte Order Settings: Compare raw register hex codes against documented field device values before enabling software byte-swapping functions.
  5. Confirm Application Logic: Ensure communication status bits enable data transfer blocks within the AC 800M controller program.

Field Installation Standards and Compliance Practices

Robust field installation prevents intermittent data corruption in factory automation networks. Signal cables must maintain proper separation from high-voltage motor wiring to prevent electromagnetic interference. Furthermore, control cabinet installations must adhere to international grounding regulations under IEC 61000 standards. Engineering teams must document all firmware revisions and Control Builder settings prior to performing hardware maintenance.

B2B Procurement and Hardware Compatibility Insights

Procurement specialists must verify hardware revisions and firmware compatibility when purchasing replacement parts. Modern CI867A modules offer enhanced diagnostics but require specific System 800xA software versions. Simply matching a base part number does not guarantee seamless hot-swapping without configuration updates. Therefore, integration teams should validate firmware compatibility before installing spare parts during planned downtime.

Application Scenario: Refined Chemical Processing Line

A chemical plant replaced a faulty CI867 module connecting an AC 800M DCS to a rack of variable speed drives. Following the replacement, all motor speed and current feedback values dropped to zero, halting production interlocks. The Ethernet Link LED remained fully operational, leading technicians to suspect a corrupt drive program.

Engineers from Powergear X Automation inspected the system and discovered that the replacement module defaulted to Function Code 04 (Input Registers), whereas the drives required Function Code 03 (Holding Registers). Reconfiguring the Control Builder hardware tree restored raw communication instantly. A minor byte-swap adjustment on 32-bit float channels then returned accurate motor current readings within 30 minutes.

For certified spare parts and expert technical support on ABB AC 800M systems, visit Powergear X Automation to secure reliable hardware solutions for your plant infrastructure.

Frequently Asked Questions (FAQ)

Q1: Does a normal Link LED mean the CI867 module is transmitting Modbus data?
No. The Link LED only confirms physical layer connection to the network switch. It does not verify IP routing, Modbus TCP handshakes, or valid register polling.

Q2: How do I determine whether I need a Byte Swap or a Word Swap?
Examine raw hexadecimal data from a known non-zero register. If the individual bytes within a 16-bit register are reversed, apply a byte swap. If two adjacent registers in a 32-bit float are transposed, apply a word swap.

Q3: Can I drop a replacement CI867 module into an existing rack without software configuration?
While the CI867 supports module replacement, the hardware revision and firmware version must match the Control Builder project requirements. Always verify project settings and firmware compatibility before commissioning.

Replace ABB PP835A HMI with Third-Party OPC Touchscreens

Replacing Damaged ABB PP835A HMI with Third-Party Touchscreens via OPC Communication

Physical damage to an ABB PP835A touchscreen panel does not force plants to replace the entire DCS architecture. Operators can retain the AC 800M controller and its core control logic. By establishing an OPC communication layer, engineers can stream process variables to third-party HMIs seamlessly. Powergear X Automation presents this guide to explain how plants can maintain system stability using modern industrial automation solutions.

Understanding MMS Communication in AC 800M Control Systems

The AC 800M controller utilizes Manufacturing Message Specification (MMS) as its primary control network protocol. ABB documentation confirms that MMS handles project downloads, online diagnostics, and alarm communications. However, standard third-party HMIs cannot natively parse MMS data structures. Simply plugging an Ethernet cable into an AC 800M controller will not grant variable access. Therefore, system integrators must bridge the gap between MMS and standard Ethernet protocols.

The Role of ABB OPC Server in Protocol Translation

The ABB OPC Server for AC 800M collects field data from the controller via MMS. It then translates these values into standard OPC DA or OPC UA interfaces. As a result, third-party platforms like Siemens WinCC or Weintek HMIs can read process tags easily. This architecture protects the core control program, eliminating the need to rewrite complex controller logic. Consequently, plants save hundreds of engineering hours during panel retrofits.

Comparing OPC DA and OPC UA for Modern Plant Architectures

Legacy DCS installations heavily rely on OPC DA, which operates on Windows DCOM technology. While OPC DA offers fast local integration, it faces severe network security limitations. Conversely, OPC UA provides cross-platform compatibility, robust encryption, and built-in user authentication. Industrial automation trends show that over 70% of new factory automation upgrades now require OPC UA. Therefore, engineers should evaluate network security requirements before selecting their integration architecture.

Step-by-Step Commissioning Procedure for HMI Replacement

  1. Audit Existing Tag Sourcing: Map all process variables, data types, and alarm states from the original PP835A project.
  2. Configure Tag Access Rights: Establish read-only permissions during initial testing to protect running production equipment.
  3. Deploy Independent Test Environment: Validate OPC Server connections and tag browsing offline before connecting to the live control network.
  4. Execute Staged Variable Testing: Verify digital status indicators, analog values, and alarm quality flags prior to enabling write commands.

Field Installation Practices and Control Network Optimization

Connecting new HMIs directly to a live control network introduces unnecessary operational risks. Continuous polling of thousands of tags can overload the AC 800M Ethernet communication modules. Engineers must optimize tag update rates based on process dynamics. For instance, temperature and tank level tags require slower scan times than fast motion loops. Moreover, field technicians must follow strict isolation practices during commissioning to prevent accidental trips.

Integrating Third-Party HMIs via OPC Gateway Architecture

Deploying a dedicated OPC Gateway creates a secure buffer between the AC 800M control network and external HMIs. The gateway retrieves data via MMS and exposes encrypted OPC UA endpoints to third-party devices. Furthermore, this architecture simplifies future plant expansions, such as integrating SCADA, Historian, or MES software. As a result, plant managers achieve a modular and scalable industrial automation infrastructure.

Application Scenario: Petrochemical Facility HMI Migration

A continuous chemical processing plant suffered a screen failure on an aging ABB PP835A panel connected to an AC 800M controller. Sourcing an exact Panel 800 replacement required a four-week lead time, threatening costly plant downtime. The engineering team deployed a third-party touchscreen HMI using the existing ABB OPC Server.

First, the team created a comprehensive Tag Mapping List to mirror the original PP835A variable addresses. Second, they configured an OPC UA client interface on the new HMI to establish secure data exchange. Finally, they conducted staged read-write validation on a isolated network segment. The new HMI went live within 48 hours without modifying a single line of AC 800M controller code.

For high-performance control system components and expert technical support on DCS migrations, visit Powergear X Automation to explore reliable hardware solutions for your plant.

Frequently Asked Questions (FAQ)

Q1: Can I connect a Siemens or Weintek HMI directly to an AC 800M without an OPC Server?
Direct Ethernet connections generally fail because standard HMIs lack native AC 800M MMS protocol drivers. You must use an ABB OPC Server, a dedicated OPC Gateway, or an HMI model with a specialized AC 800M driver.

Q2: Do I need to reprogram the AC 800M controller when replacing the PP835A?
No. The core control program remains untouched. You only need to map the new HMI tags to the process variables already published by the controller or OPC Server.

Q3: What causes write failure when controlling pumps or valves from a new HMI?
Write failures usually result from incorrect DCOM security settings in OPC DA, misconfigured user permissions in OPC UA, or tag data type mismatches between the HMI and the OPC Server.

Fix GE Fanuc IC695CPE305 CPU Random Reboots | RX3i Guide

Why GE Fanuc IC695CPE305 CPUs Experience Random Reboots and How to Fix Them

In modern industrial automation, unexpected controller reboots cause severe operational downtime. The GE Fanuc PACSystems RX3i IC695CPE305 CPU serves as a core processing unit in complex factory automation systems. However, field engineers often report random CPU reboots after approximately two years of continuous operation. Powergear X Automation provides this practical engineering guide to diagnose root causes, eliminate recurring downtime, and optimize PLC stability.

Analyzing Power Supply Degradation and Transient Dips in DCS Architecture

Power quality issues represent the primary trigger for spontaneous PLC reboots. Although power supply units work reliably at installation, internal capacitors degrade gradually over time. Consequently, high-current switching events from nearby heavy motors create momentary voltage sags. These micro-second voltage dips bypass standard multimeters but trigger the CPU under-voltage protection circuit. Therefore, maintenance teams must capture real-time power waveforms using a high-speed oscilloscope before replacing hardware.

Evaluating Thermal Stress and Long-Term Cabinet Enclosure Conditions

Heat accumulation degrades delicate microelectronics inside programmable logic controllers. Enclosure filters clog with industrial dust after extended operation without regular maintenance. As a result, internal cabinet temperatures steadily climb beyond the recommended 60°C operating limit. Excess heat triggers thermal protection mechanisms inside the CPU processor. Moreover, long-term thermal expansion loosens backplane connectors, creating intermittent physical connection drops during peak operational shifts.

Investigating CPU Firmware Restrictions and Software Watchdog Events

Software anomalies frequently mimic hardware failures in modern control systems. According to industrial control industry surveys, over 30% of unexpected PLC restarts originate from software watchdog timeouts. Heavy non-volatile memory write operations or unhandled system interrupts lock up the execution thread. Consequently, the internal watchdog timer resets the CPU to prevent erratic machine behavior. Engineers must analyze the PAC Machine Edition fault table before clearing CPU error logs.

Step-by-Step Diagnostic Sequence for Resolving CPE305 Reboots

  1. Preserve Diagnostic Error Tables: Connect to the CPU via PAC Machine Edition immediately and export the complete controller fault log.
  2. Monitor DC Power Quality: Install a transient power recorder to log 24V DC bus stability during heavy motor startup sequences.
  3. Inspect Physical Connections: Check backplane connectors, terminal blocks, and Energy Pack module cables for corrosion or mechanical looseness.
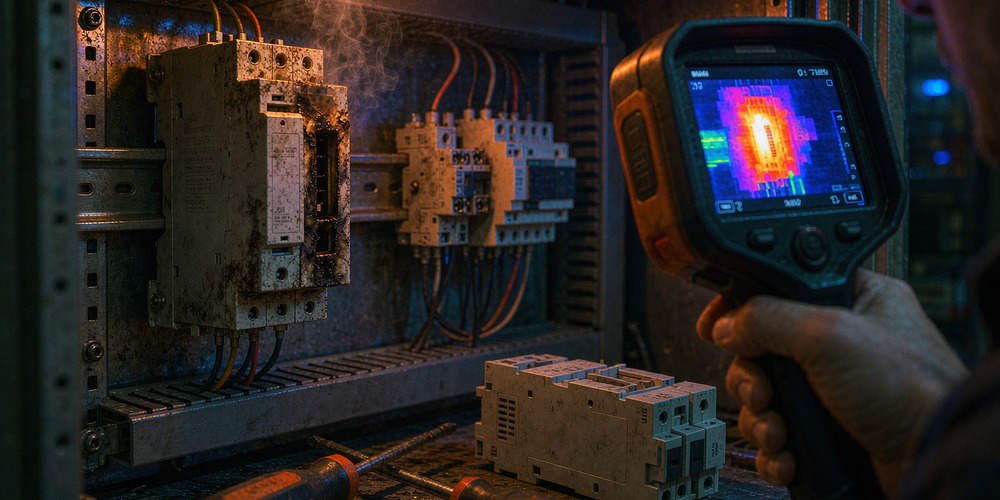
  4. Verify Cabinet Thermal Profile: Measure internal panel temperatures using thermal imaging cameras under full operational loads.

Inspecting Energy Pack Performance and Power Loss Backup Systems

The IC695CPE305 processor utilizes an Energy Pack capacitor module to preserve volatile RAM data during power outages. However, aging Energy Pack units can develop internal short circuits or fail to maintain adequate charge holding capacity. When an unstable Energy Pack draws excessive current from the CPU internal rail, it induces voltage drops across the processor board. Therefore, field technicians should regularly test and replace aging backup energy modules according to manufacturer maintenance schedules.

B2B Procurement Strategies and Backward Compatibility Verification

Replacing an IC695CPE305 module requires careful compatibility evaluation rather than quick component swapping. System integrators must verify CPU hardware revisions, installed firmware builds, and backplane bus speeds. While modern Emerson RX3i controllers support legacy Series 90-30 I/O modules, firmware mismatches can cause backplane communication errors. Procurement managers must review technical specifications thoroughly before scheduling system upgrades during maintenance windows.

Application Scenario: Chemical Plant Processing Line Recovery

A continuous chemical processing plant experienced random IC695CPE305 reboots every few days, interrupting critical batch mixing operations. The maintenance team initially suspected a defective CPU board and replaced the hardware, yet the reboots persisted. Powergear X Automation specialists audited the panel installation and discovered that aging panel cooling fans had failed, causing internal enclosure temperatures to reach 68°C.

The engineering team installed new cabinet ventilation fans and cleaned the clogged dust filters. Additionally, they updated the CPU firmware to the latest revision and adjusted the power supply monitoring parameters. These targeted actions reduced panel temperatures to a stable 38°C, completely eliminating random CPU reboots and restoring 100% processing line uptime.

To source reliable GE Fanuc PACSystems RX3i components and receive expert technical troubleshooting support, visit Powergear X Automation today for your factory automation needs.

Frequently Asked Questions (FAQ)

Q1: Should I immediately replace my IC695CPE305 CPU when random reboots start?
No. You should first investigate external power supply dips, cabinet overheating, and backplane looseness. Replacing the CPU will not resolve external electrical or thermal issues.

Q2: How does the Energy Pack affect CPU boot behavior on the PACSystems RX3i?
The Energy Pack powers the CPU memory save process during shutdown. A degraded or shorted Energy Pack can cause startup faults or force the CPU into reboot loops.

Q3: What tools are required to capture voltage transients causing PLC reboots?
Standard multimeters are too slow to detect millisecond voltage sags. You need a digital storage oscilloscope or a specialized power quality analyzer to capture brief DC power dips.

Troubleshoot Honeywell XNX Gas Detector Blank Display Errors

Troubleshooting Honeywell XNX Gas Detector Blank Display: Display Module or Main Board Failure?

A Honeywell XNX Universal Gas Detector may keep its green power LED lit while the LCD screen turns completely blank. However, this condition does not automatically indicate a defective main board. Faults often originate from the display assembly, internal power supply, or ribbon cable connection. Powergear X Automation presents this technical troubleshooting guide to isolate gas detection faults efficiently without replacing expensive electronic assemblies unnecessarily.

The Operational Importance of Local Gas Detector Displays

Industrial facilities rely on Honeywell XNX gas detectors to provide immediate toxic or flammable gas measurements. Local LCD displays allow operators to view gas concentrations, diagnostic faults, and calibration status directly in hazardous areas. When the screen turns blank, operators lose real-time local visibility. According to industrial safety field reports, quick fault isolation reduces system downtime significantly. Therefore, field technicians must isolate display failures from core processing issues before ordering replacement components.

Power LED Status Does Not Prove Display Circuit Health

An illuminated green power LED simply confirms that the primary 24V DC supply reaches the transmitter terminals. However, it does not guarantee that the internal 3.3V DC LCD rail operates correctly. The main board converts input power through separate step-down regulators to drive the display processor and backlight. Consequently, a faulty internal power converter can freeze the screen while the power LED stays lit. Technicians must check secondary voltage rails before assuming total main board failure.

Evaluating Communication Interfaces to Verify Main Controller Health

Technicians should check whether the main processor continues to communicate with central control systems. If the transmitter sends valid 4-20mA signals or responds to HART handheld communicators, the main board remains functional. Therefore, active fieldbus or DCS communications confirm that the central processor is executing its code. In this scenario, the failure isolates directly to the display POD assembly, ribbon cable connector, or local LCD driver circuit.

Key Compatibility Factors Before Ordering XNX Replacement Components

Honeywell XNX gas detectors feature modular hardware architectures with various personality and option boards. Purchasing a replacement display module based solely on the enclosure appearance often leads to compatibility issues. Technicians must verify the complete model configuration code, PCB revision, and firmware version before purchasing hardware. Furthermore, hardware substitutions in hazardous locations must strictly adhere to ATEX or IECEx certified maintenance guidelines.

Step-by-Step Diagnostic Sequence for Fault Isolation

  1. Check Communication Status: Connect a HART communicator or monitor the DCS 4-20mA input channel to verify processor activity.
  2. Isolate Power and Inspect Cabling: De-energize the unit, open the flameproof enclosure, and inspect the internal ribbon cables for corrosion.
  3. Verify Internal Voltage Rails: Apply power safely and measure the secondary internal 3.3V DC test points using an approved multimeter.
  4. Perform Controlled Component Substitution: Install a known-good compatible display POD assembly to observe whether normal screen function resumes.

Environmental Hazards Impacting Gas Detection Electronics

Industrial plants expose field electronics to extreme environmental stresses over extended operational cycles. Heavy vibration from nearby pumps or compressors can loosen internal ribbon cable connectors over time. Moreover, thermal cycling and high humidity encourage moisture condensation inside the housing, causing micro-corrosion on delicate display pin headers. Installing high-quality seals and applying recommended terminal torque specifications prevents environmental damage effectively.

Procurement Guidance and B2B Cost Optimization

Ordering a full main transmitter assembly for a simple LCD display failure increases maintenance costs substantially. Procurement managers should establish spare parts inventories based on component-level failure rates. Sourcing individual display modules or personality boards reduces emergency repair budgets dramatically. However, buyers must ensure that suppliers verify exact hardware revision compatibility before dispatching replacement components.

Application Scenario: Offshore Platform Gas Detector Maintenance

An offshore oil platform reported a blank LCD screen on an XNX transmitter monitoring hydrogen sulfide near a compressor skid. The power LED remained green, but operators could not perform local zero calibrations. Replacing the entire transmitter housing would require a lengthy hot-work permit and system shutdown.

The instrument team connected a HART communicator and confirmed that the transmitter was actively sending a normal 4.0mA signal to the DCS. By executing a controlled display POD substitution during scheduled maintenance, the team restored the display in fifteen minutes. This targeted repair saved thousands of dollars in downtime and preserved the original explosion-proof enclosure seals.

For high-reliability gas detection components, spare parts, and expert automation support, visit Powergear X Automation to explore our extensive inventory of field instrumentation solutions.

Frequently Asked Questions (FAQ)

Q1: Does a blank XNX LCD screen mean the 4-20mA alarm output has failed?
Not necessarily. If the main processor remains active, the transmitter will continue outputting valid 4-20mA gas readings and trigger remote alarms normally despite the blank local display.

Q2: Can I swap an XNX display module without turning off the power?
No. You must de-energize the transmitter before opening the explosion-proof housing or disconnecting internal electronics to prevent electrical arcing in hazardous environments.

Q3: What causes an XNX display to freeze or show scrambled characters?
Scrambled characters usually result from electromagnetic interference (EMI), loose ribbon cable connections, or momentary voltage dips on the internal 3.3V DC power rail.

Back to Top
Product has been added to your cart