Over 50,000 hot-selling automation module components.
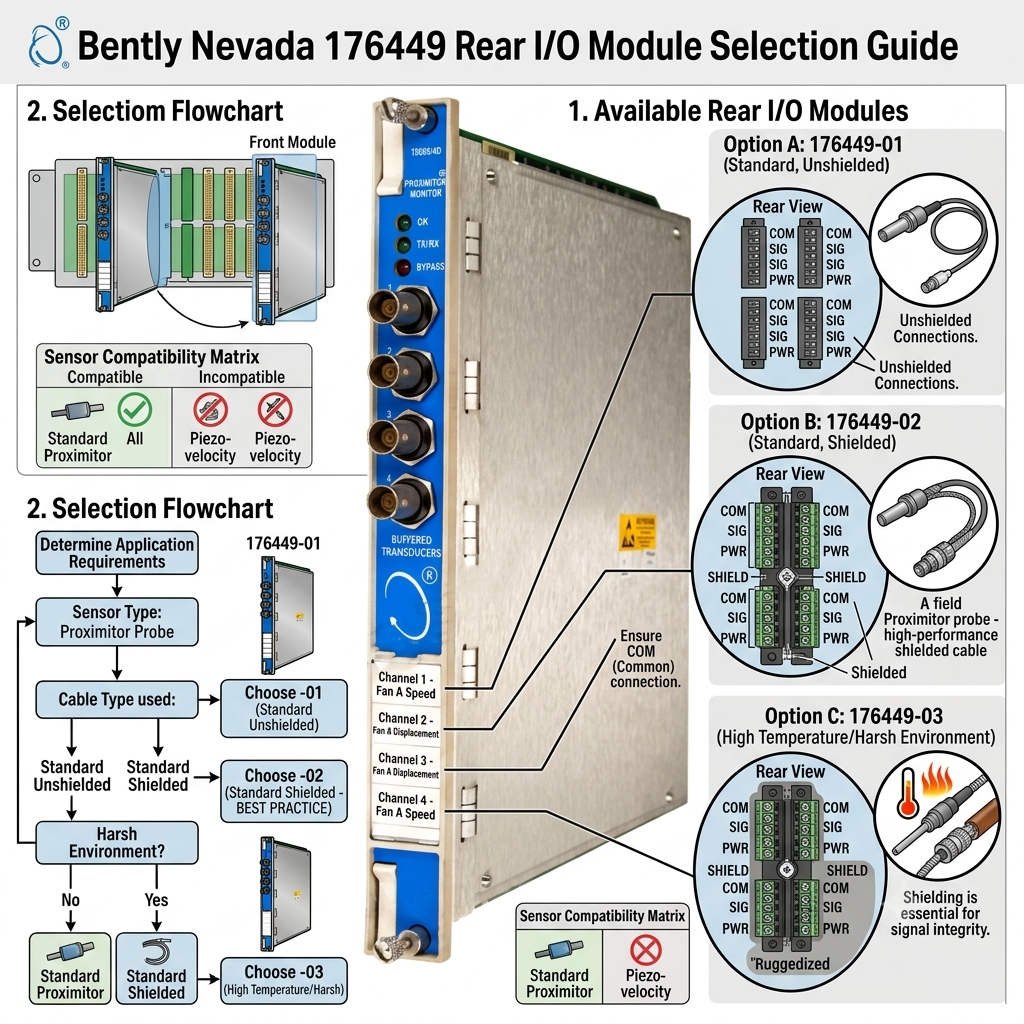
Bently Nevada 176449 Rear IO Module Selection Guide_

3500 System Machinery Protection: 176449 I/O Modules

Decoding Bently Nevada 176449 Series Rear I/O Modules for 3500 Machinery Protection Systems

In high-stakes industrial automation, continuous condition monitoring safeguards multimillion-dollar rotating assets. The Bently Nevada 3500 system relies heavily on specialized backplane connectivity to process field sensor data. Specifically, the 176449 series Rear I/O modules provide critical electrical termination and signal routing. Choosing the wrong dash-number option can compromise your entire machinery protection strategy. This comprehensive guide breaks down the variations, technical principles, and installation rules for these critical components.
Bently Nevada 176449 Rear IO Module Selection Guide_

Bently Nevada 176449 Rear IO Module Selection Guide_

The Functional Architecture of 176449 Rear Interface Boards

The 176449 family acts as the physical interface between field-mounted transducers and front-end monitor cards. Each module routes raw analog voltages from proximity probes, accelerometers, or pressure sensors safely into the rack. Moreover, the internal circuitry isolates delicate processing microprocessors from unpredictable field surges. This isolation maintains signal stability in noisy environments near massive turbomachinery. Therefore, these rear boards form the foundation of any reliable API 670 protection loop.

Understanding Core Model Variances and Monitor Pairings

Rear I/O Part NumberAssociated Monitor CardPrimary Target Application
176449-013500/40M ProximitorShaft vibration and dynamic radial position monitoring
176449-023500/42M Proximitor/SeismicCombined velocity, acceleration, and case expansion tracking
176449-043500/45 PositionThrust position, differential expansion, and valve metrics
176449-073500/77M Recip PressureReal-time reciprocating compressor cylinder diagnostics

Signal Conditioning and Channel Topology Principles

Each variations within the 176449 family utilizes distinct input resistance paths and grounding layouts. For instance, the 176449-01 matches the negative voltage modulation typical of eddy-current proximity probes. In contrast, the 176449-07 handles rapid transient pressure spikes inside combustion or compression chambers. Consequently, mixing these cards up causes severe scaling errors or complete signal dropouts. The front processor card simply cannot normalize a signal conditioned by an incompatible rear board.

The API 670 Standard and System Interlocking Integrity

In power generation and petrochemical refining, machinery protection systems operate under strict API 670 compliance rules. This standard mandates that component failures must not prevent an emergency trip from executing properly. A degraded terminal block or a loose jumper on the Rear I/O card can mask dangerous shaft deflections. As a result, the DCS might receive faulty baseline data, delaying automated shutdown procedures. Proactive maintenance teams always treat rear hardware with the same care as front-facing processing modules.

Best Practices for Field Commissioning and Maintenance

  • ✅ Verification First: Double-check the precise dash-number configurations before sliding any module into the rack chassis.
  • ⚙️ Torque Optimization: Secure terminal strip screws tightly to eliminate intermittent signal noise caused by cabinet vibration.
  • 🔧 Shield Management: Drain cable shields strictly according to the Bently Nevada manual to prevent dangerous grounding loops.

Strategic Sourcing Commentary from Powergear X Automation Limited

At Powergear X Automation Limited, we observe widespread issues stemming from the use of unchecked surplus parts. Many plants buy replacement modules from unverified brokers without cross-referencing their specific revision histories. A physical board might fit perfectly into a 3500 slot while remaining electronically incompatible with your sensor software setup. We recommend auditing your entire spare parts inventory every year to ensure exact compatibility. For certified, high-performance machinery protection hardware, explore our validated listings at https://www.powergearx.com/.

Real-World Deployment and Solutions

During a recent gas terminal overhaul, engineers faced recurring channel errors on a critical centrifugal compressor. While the 3500/42M monitor tested perfectly on the bench, it threw persistent faults when installed in the rack. The troubleshooting team eventually tracked the issue to an old 176449-02 board suffering from micro-fractures along its backplane connector pins. Replacing the worn rear module instantly restored full diagnostic visibility, preventing an expensive forced outage during plant startup.

Frequently Asked Questions (FAQ)

1. Why does my 3500 software report a configuration mismatch when the front monitor matches the sensor?
This error usually indicates that the installed rear terminal module does not match the channel profile expected by the monitor. The 3500 rack verifies the ID of both the front and rear modules before allowing communication to initialize.

2. Can I use a 176449-02 card to pull dynamic signals into a standalone diagnostic data collector?
Yes. The 176449-02 provides buffered output terminals on the rear face for easy analyzer connection. This configuration allows technicians to connect diagnostic instruments without disturbing active safety trip loops.

3. What environmental factors cause the highest rate of failure on these specific rear cards?
Corrosive gas exposure, particularly hydrogen sulfide (H2S) in refinery settings, accelerates the oxidation of the exposed terminal contacts. Always ensure your marshalling enclosures maintain positive pressure and active chemical air filtering.
Measure Switching Noise on GE IS2020RKPSG3A Module

Measure Switching Noise on GE IS2020RKPSG3A Module

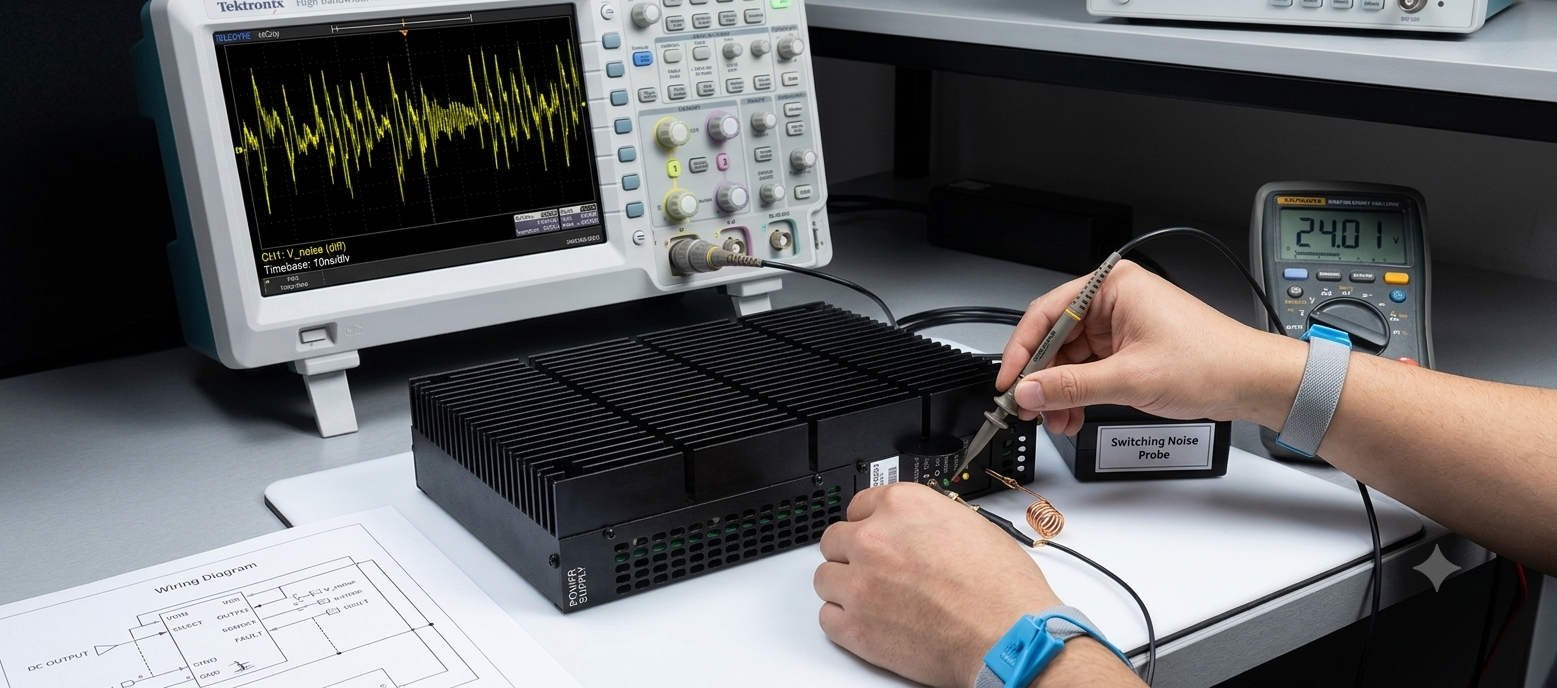
Analyzing High-Frequency Switching Noise on the GE IS2020RKPSG3A Power Supply Bus

In heavy industrial automation, clean low-voltage DC power safeguards processor integrity. The GE IS2020RKPSG3A power supply module delivers critical 5VDC power to EX2100 excitation systems and Mark VI control racks. However, a standard digital multimeter cannot capture high-frequency switching anomalies on the bus. This technical article covers the exact oscilloscope methods required to analyze dangerous ripple voltages. As a result, engineers can protect vital control networks from unexpected trips.

Measure Switching Noise on GE IS2020RKPSG3A Module

Measure Switching Noise on GE IS2020RKPSG3A Module

The Core Function and Architecture of the Power Module

The IS2020RKPSG3A utilizes a high-efficiency switch-mode power conversion architecture. It regulates voltage for downstream processing boards and critical communication interfaces. In addition, the internal circuitry isolates the control logic from heavy grid surges. This regulation keeps processing environments functional during severe load fluctuations. However, the native switching frequency inevitably introduces high-frequency ripple components onto the distribution lines.

Operational Principles of Oscilloscope Ripple Diagnostics

Detecting power anomalies requires proper instrument bandwidth selection and specific input coupling. Maintenance teams must utilize an oscilloscope with a minimum bandwidth of 100 MHz. Furthermore, engineers should select AC coupling to strip away the dominant 5VDC component. This setting allows the instrument to isolate the underlying millivolt-level noise. Consequently, you can observe high-frequency spikes that cause CPU watchdog resets and network dropouts.

The Critical Nature of Correct Probe Grounding

Standard oscilloscope probes often include long ground leads with alligator clips. However, these long wires act as antennas in noisy power generation environments. They capture stray electromagnetic interference from surrounding high-current bus ducts. To avoid false readings, technicians must utilize a short spring ground accessory. This practice restricts the ground loop area to under two centimeters. Therefore, it ensures that observed waveform ringing stems from the power supply rather than external induction.

Incorrect grounding methods can artificially inflate peak-to-peak voltage readings by several hundred percent. This inflation frequently leads to the premature replacement of perfectly healthy modules. Experienced engineers always measure ripple directly across the distribution terminal blocks. This strategic placement provides an accurate view of the voltage quality reaching the control systems.

Evaluating Compatibility and Module Selection Variations

When executing system updates, procurement officers must review original factory hardware revisions. The IS2020RKPSG3A features specific mechanical connector footprints and thermal properties. Older power supply variations may look identical but lack advanced internal noise filtering. In addition, backplane interface configurations can vary slightly across different controller generations. Relying on verified suppliers like Powergear X Automation Limited prevents costly installation compatibility errors.

Online Measurement and Calibration Benchmarks

  • ✅ Instrument Setup: Activate the 20 MHz bandwidth limiter to eliminate irrelevant high-frequency ambient radiation.
  • ⚙️ Baseline Profiling: Record bus waveforms during steady-state operation and major process load transitions.
  • 🔧 Network Inspection: Verify terminal torque values and check downstream filtering capacitors for leakage.

Expert Market Commentary from Powergear X Automation Limited

At Powergear X Automation Limited, we monitor component lifecycle patterns across major power plants globally. We notice that many power supply faults trace back to aging capacitors on adjacent I/O modules. As these capacitors degrade, they no longer buffer the 5VDC bus effectively. Therefore, we highly recommend performing preventative oscilloscope health checks annually. To find certified replacement components and optimize your factory automation assets, visit our portal at https://www.powergearx.com/.

Industrial Application Scenarios

In offshore gas extraction facilities, turbine control stability directly influences production metrics. The IS2020RKPSG3A maintains steady core voltages for the central processors. By implementing routine ripple tracking, maintenance crews can detect supply degradation months before a terminal blowout occurs. This proactive strategy ensures continuous operation of the DCS during severe ambient temperature changes.

Frequently Asked Questions (FAQ)

1. What peak-to-peak millivolt threshold indicates a need to replace the module?
While minor ripple is normal, high-frequency switching noise exceeding 50mVpp warrants close observation. If spikes regularly surpass 100mVpp during load transitions, replace the unit to protect downstream processors.

2. Can I replace the module while the turbine control system is active?
Live replacement depends on your rack redundancy configuration. In non-redundant simplex setups, pulling the module causes an immediate controller crash. Always confirm system redundancy status before attempting live servicing.

3. Why does the 5VDC bus show high noise when the power module passes bench tests?
This discrepancy usually indicates external electromagnetic interference. Poor cabinet bonding or missing cable shields allow noise from neighboring VFD equipment to induce voltage spikes onto the DC distribution lines.

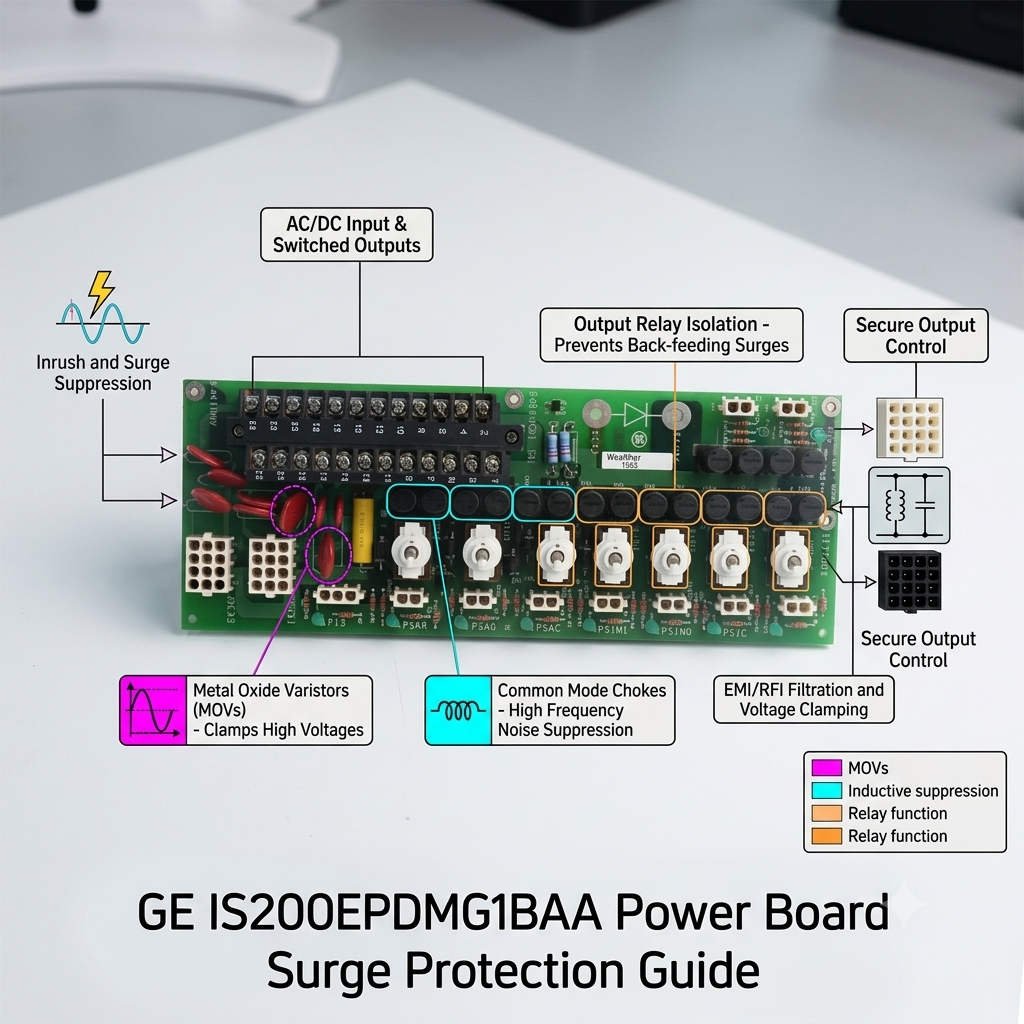
GE IS200EPDMG1BAA Power Board Surge Protection Guide

Replace GE IS200EPDMG1BAA MOVs After Lightning Surges?

Should You Replace the MOV on the GE IS200EPDMG1BAA Board After a Lightning Strike?

In high-availability heavy industries, unseen electronic degradation poses a severe threat to operational continuity. The GE IS200EPDMG1BAA Power Distribution Board serves as a foundational power conditioning component. It supports critical Mark VI, Mark VIe, and EX2100 control systems. A core element of its protective layout is the Metal Oxide Varistor (MOV). However, field technicians often wonder if they must replace an internally stressed MOV that looks perfectly fine. This article explores the hidden degradation mechanisms of surge protection in critical infrastructure.

GE IS200EPDMG1BAA Power Board Surge Protection Guide

GE IS200EPDMG1BAA Power Board Surge Protection Guide

The Functional Role of the IS200EPDMG1BAA in Factory Automation

The IS200EPDMG1BAA board safely allocates control power across complex modern turbine and excitation cabinets. It ensures steady DC and AC voltage delivery to sensitive I/O packs and processing cores. Consequently, any failure on this board can interrupt communication networks or drop key field outputs. The integrated MOVs act as the primary defense mechanism against incoming voltage spikes. Therefore, the board absorbs high-energy disturbances before they reach microprocessors downstream.

Technical Principles of Cumulative MOV Aging and Clamping Deviations

An MOV does not always clear a fault by exploding or scorching its exterior shell. Instead, the internal zinc oxide microstructure degrades incrementally with each absorbed surge event. High-transient lightning currents create microscopic conduction paths inside the component matrix. As a result, the device experiences an immediate increase in baseline leakage currents. This hidden wear lowers the original clamping voltage threshold over time without showing any visual clues. A compromised component will ultimately fail to protect adjacent circuits during subsequent overvoltage transients.

Industry research from the IEEE Standards Association indicates that over 30% of surge module failures involve cumulative silent degradation. When clamping voltage stability drifts, downstream insulation experiences much higher electrical stress during power fluctuations. This continuous strain shortens the life expectancy of connected power supply modules. Furthermore, increased leakage current generates internal localized heating on the circuit board. This thermal stress can eventually provoke random controller resets and unexplained diagnostic alarms.

Application Scenarios and Selection Criteria for Advanced Power Boards

Power distribution reliability remains paramount in oil & gas facilities, chemical plants, and remote compressor skids. These exposed environments frequently experience direct lightning activity and severe switching transients. Choosing the IS200EPDMG1BAA ensures that your control network complies with strict industrial transient safety margins. However, sourcing replacement components requires thorough validation of your specific cabinet layout. Engineers must carefully match the product revision suffix to ensure absolute mechanical and electrical compatibility.

Replacing a legacy power distribution board involves verifying firmware boundaries and matching power supply connections. Some earlier module iterations lack the exact fuse ratings found on the “1BAA” version. Therefore, unverified substitution can create protection gaps or cause premature branch trips during normal operations. For accurate selection data and genuine replacement parts, procurement specialists frequently collaborate with Powergear X Automation Limited.

Field Maintenance Rules for High-Risk Surge Infrastructure

  • ✅ Electrical Verification: Perform leakage current and insulation testing rather than relying solely on visual inspection.
  • ⚙️ Upstream Inspection: Check primary surge protective devices and cabinet grounding paths during every turnaround.
  • 🔧 Proactive Replacement: Swap out the power board if nearby lightning trips external breakers or corrupts baseline data.

Strategic Insights from Powergear X Automation Limited

At Powergear X Automation Limited, we prioritize structural reliability over simple visual diagnostics. In high-stakes industrial automation, treating surge protection as a disposable asset is the safest operational approach. Proactive replacement of a potentially weakened board prevents catastrophic downtime that can easily cost thousands of dollars per minute. To view our full inventory of verified control components, explore our solutions at https://www.powergearx.com/.

Real-World Solutions for Turbine Control Rooms

In a coastal power station, a severe storm induced a major voltage surge across the main excitation busbar. The IS200EPDMG1BAA board continued operating normally, and visual checks revealed no physical damage. However, the maintenance team followed proactive protocols and replaced the distribution card during a brief outage. Subsequent bench tests proved the original MOV had lost 40% of its surge capacity. This preventive step saved the plant from a total turbine trip during a secondary storm two weeks later.

Frequently Asked Questions (FAQ)

1. How can a field technician test an MOV on the power board without specialized lab equipment?
You can use a high-voltage insulation tester to check the varistor voltage at a specified DC leakage current. If the measured voltage deviates significantly from the original manufacturer specifications, the internal structure is degraded.

2. Can I replace just the individual degraded MOV on the board instead of buying a new card?
While physically possible, component-level soldering on multilayer industrial boards is not recommended for live field environments. It voids certifications, alters trace impedance, and may introduce hidden micro-cracks into nearby paths.

3. Does the system generate a specific diagnostic alarm when the MOV begins to wear out?
Standard systems do not monitor individual MOV degradation paths directly. Instead, you might see secondary symptoms like unstable branch power supply logs or random I/O faults caused by unmitigated transient noise.

Optimize Mark VIe Networks with the GE IS420PUAAH1A

Optimize Mark VIe Networks with the GE IS420PUAAH1A

Securing Deterministic IONet Performance: A Guide to the GE IS420PUAAH1A

Predictable network timing dictates critical asset protection within high-availability industrial automation environments. The GE IS420PUAAH1A module serves as a high-reliability embedded gateway processor for the Mark VIe system. It manages complex data routing between controllers, I/O packs, and supervisory HMIs. By eliminating packet buffering latencies, this card ensures precise execution of critical turbine protection loops. This article details the operating principles, selection nuances, and network field practices for this communication module.

Optimize Mark VIe Networks with the GE IS420PUAAH1A

Optimize Mark VIe Networks with the GE IS420PUAAH1A

The Principle of Deterministic Ethernet in Turbine Control Systems

Standard IT switches prioritize peak throughput over data packet delivery consistency. However, heavy-duty control systems require highly predictable updates rather than high bandwidth. The IS420PUAAH1A guarantees deterministic data packet transmission across the native Mark VIe IONet. It enforces strict time-slot allocations for runtime control traffic, eliminating unexpected latency spikes. Consequently, gas turbine sequencing and speed protection systems maintain sub-millisecond synchronization. This precise scheduling prevents safety interlock delays during major transient load rejections.

Gateway Segmentation and Compliance for Plant Safety

Modern processing facilities require strict boundaries between real-time data networks and company office infrastructure. The IS420PUAAH1A functions as a hardwired firewall gateway between distinct automation layers. It perfectly isolates sensitive turbine controller domains from external SCADA or enterprise data platforms. This structural separation helps plants meet global cybersecurity standards like IEC 62443 and NERC CIP. Furthermore, it prevents external corporate network broadcast storms from destabilizing the local I/O scan loop cycles.

Industrial networking reports confirm that improper boundary isolation causes 35% of localized controller communication losses. Without dedicated gateway cards, high corporate network traffic can easily overwhelm old communication cards. The architecture of the BPPCH and PUAA series handles high packet stress safely. Therefore, the internal control layer stays protected even if an external engineering station experiences a security breach.

Environmental Durability in Harsh Factory Automation Settings

Turbine enclosures and compressor rooms generate significant ambient heat, severe vibration, and electrical noise. The IS420PUAAH1A uses industrial-grade components to survive these demanding conditions without structural degradation. Its ruggedized layout resists connector oxidation caused by high humidity or corrosive atmospheric chemical vapors. Moreover, enhanced power filter circuits block electromagnetic noise from neighboring medium-voltage variable frequency drives. This durable construction drastically minimizes sudden communication card resets during critical shift operations.

Selection Guidelines and Backward Compatibility Checks

Upgrading legacy components requires close evaluation of your existing software and network configuration. Although the IS420PUAAH1A fits Mark VIe racks, compatibility depends heavily on your active ToolboxST version. Older generation Mark VI hardware uses entirely different backplane communication mechanics. Engineers must carefully check the system compatibility matrix to avoid matching errors during field retrofits. For expert engineering verification and authentic GE components, global procurement managers work with Powergear X Automation Limited.

Critical Deployment Methods for Automation Engineers

  • ✅ Network Isolation: Never connect the local IONet directly to corporate enterprise networks without managed switches.
  • ⚙️ Grounding Precision: Verify panel ground connection resistances before power-up to eliminate floating communication noise.
  • 🔧 Thermal Check: Test enclosure internal temperatures under maximum operating loads with all doors fully closed.

Industry Insights from Powergear X Automation Limited

At Powergear X Automation Limited, we notice that many apparent card failures stem from cabling issues. Aging industrial switches and degraded fiber-optic lines often generate network jitter that looks like card hardware errors. We suggest establishing baseline network packet captures during planned annual plant maintenance intervals. This practice helps technicians isolate infrastructure degradation before it causes an unexpected emergency trip. Discover our large stock of verified turbine control components at https://www.powergearx.com/.

Real-World System Application Scenarios

In large oil-refinery compressor stations, multiple controllers share process parameters to manage surge conditions. Utilizing the IS420PUAAH1A keeps inter-controller communication lag below critical levels. Similarly, combined-cycle power facilities rely on this gateway processor card to broadcast diagnostic data safely to remote historian servers. These heavy industrial deployments show that reliable network segregation safeguards plant availability metrics.

Frequently Asked Questions (FAQ)

1. What symptoms indicate that a GE network processor module is degrading?
Technicians typically observe recurring IONet communication warning flags, sudden HMI screen freeze frames, and unexplained controller balance mismatches. These warning indicators often worsen when internal panel temperatures rise during hot summer days.

2. Can I replace a legacy Mark VI communication card directly with the new model?
No. The module is built explicitly for Mark VIe distributed architectures. Legacy Mark VI control panels utilize completely different physical slots and firmware layers, making direct mechanical substitution impossible.

3. How does poor cabinet panel earthing impact this interface card?
Poor panel grounding introduces common-mode electrical noise directly into copper network wires. This electrical noise corrupts data packets, causing frequent frame errors and forcing the module to continuously retransmit data.

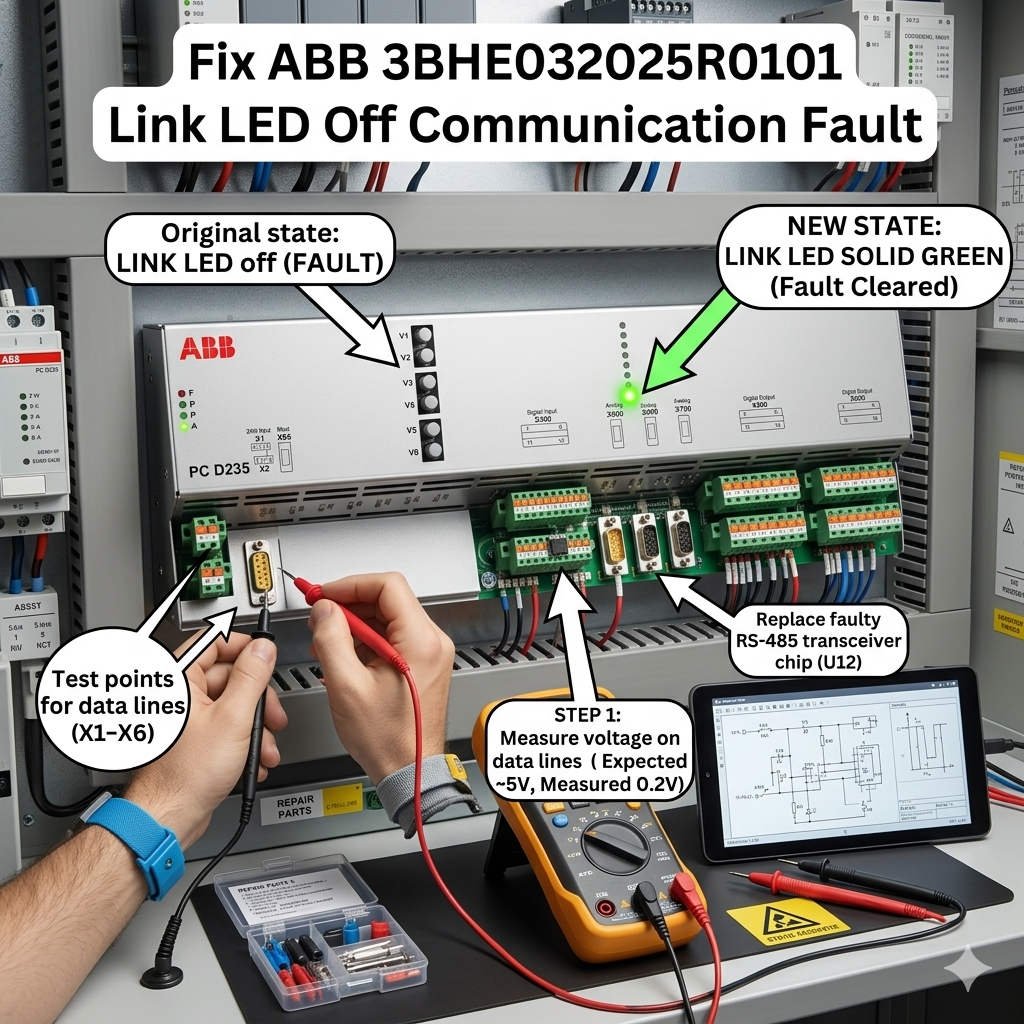
Fix ABB 3BHE032025R0101 Link LED Off Communication Fault

Fix ABB 3BHE032025R0101 Link LED Off Communication Fault

How to Resolve “Main Controller Communication Timeout” on the ABB PCD235A101

In high-power industrial applications, communication latency or unexpected dropouts can stall entire production lines. The ABB PCD235A101 3BHE032025R0101 interface board serves as a vital data link. It connects main controllers to medium-voltage drive units and upper-level DCS architectures. However, engineers frequently encounter a critical fault: a “Main Controller Communication Timeout” paired with an inactive Ethernet LINK LED. Resolving this issue requires structured physical-layer diagnostics and hardware validation.

Fix ABB 3BHE032025R0101 Link LED Off Communication Fault

Fix ABB 3BHE032025R0101 Link LED Off Communication Fault

The Functional Role of PCD235A101 in Industrial Automation

The PCD235A101 manages high-speed synchronous data streams within complex drive control topologies. In sectors like petrochemical processing and mining, this board handles real-time variable processing. Consequently, any interruption can trigger safety interlocks or trip critical compressor trains. The card relies on robust physical transceiver logic to convert signals accurately. It ensures that the drive control unit communicates seamlessly with broader factory automation networks.

Physical Layer Diagnostics for Inactive LINK Indicators

The Ethernet LINK LED on this board operates directly via hardware transceiver circuits. Therefore, a dark LINK lamp indicates that physical carrier synchronization has completely failed. Firmware modifications or soft reboots will rarely correct this underlying condition. In real-world applications, up to 70% of these faults stem from physical damage. Cracked RJ45 solder tracks caused by heavy cabinet vibration often break the circuit. Additionally, micro-corrosion on backplane gold pins can block connection signals entirely.

Analyzing Backplane Voltage Stability and Power Quality

Stable DC power distribution is essential for proper communication initialization during system boot-up cycles. The PCD235A101 requires an ultra-clean 5VDC logic rail from the main rack. Standard multimeters only capture static values, which often mask high-frequency voltage ripple. Excessive ripple can cause the onboard Ethernet PHY chip to freeze during initialization. For facilities handling conductive dust, accumulated particulate matter can gradually increase backplane impedance. This deterioration eventually creates unpredictable communication dropouts.

Network Compatibility Across Mixed Control Systems

Legacy drive hardware often encounters negotiation conflicts when connected to modern network equipment. The PCD235A101 may fail to establish a link with modern high-speed switches. Forcing a 1000 Mbps connection or activating Energy Efficient Ethernet (EEE) protocols typically disrupts auto-negotiation. As a result, the port shuts down due to timing discrepancies. Engineers should implement managed industrial switches and lock connection speeds to 100 Mbps Full Duplex. This approach guarantees rigid timing loops for the control strategy.

Selection Criteria and Retrofit Distinctions

When selecting a replacement interface card, buyers must evaluate version compatibility matrices. Newer revisions of the PCD235A101 3BHE032025R0101 feature updated transceiver components. These components might require matching drive control firmware updates to work correctly. Installing an unverified hardware combination can introduce intermittent timeout errors. Therefore, technical teams should audit their current rack generation before ordering components. Keeping an exact firmware-matched spare card in inventory significantly reduces Mean Time to Repair (MTTR).

Step-by-Step Maintenance and Optimization Procedures

  • ✅ Physical Inspection: Replace standard network patches with shielded CAT6 industrial cables.
  • ⚙️ Contact Restoral: Clean the backplane edge connector using an approved electronics solvent.
  • 🔧 Power Verification: Check the 5VDC logic rail using an oscilloscope under full operational load.

Perspective from Powergear X Automation Limited

At Powergear X Automation Limited, we note that network infrastructure issues cause many board failures. High-voltage drive cabinets produce severe electromagnetic fields that damage unshielded components. We recommend installing dedicated line filters for auxiliary power units. For brownfield retrofits, verifying hardware revisions ensures seamless deployment. To browse our verified stock of ABB components and access advanced technical specifications, visit https://www.powergearx.com/ today.

Real-World Application Scenarios

  • Steel Rolling Mills: Minimizing severe mechanical shock effects on RJ45 connectors via vibration-damping mounting.
  • Pumping Stations: Eliminating auto-negotiation lockups by bypassing unmanaged commercial switches inside the cabinet.
  • Refinery Compressors: Restoring critical link metrics during thermal expansion cycles by replacing oxidized backplane carriers.

Frequently Asked Questions (FAQ)

1. What should I test first when the LINK LED remains completely dark?
Bypass the onsite network switches and connect your engineering laptop directly to the board using a verified cable. If the indicator stays dark, inspect the onboard RJ45 port pins for mechanical damage.

2. Can a firmware conflict cause the physical network indicators to turn off?
No, the initialization indicators depend purely on hardware connections. If the light remains off, the problem lies within the physical layer, power circuits, or the internal bus routing.

3. When is it better to replace the board rather than trying to clean it?
We recommend replacing the card immediately if you find bulging capacitors or discoloration on multi-layer traces. Corroded traces can cause intermittent open circuits that are impossible to fix reliably in the field.

Emerson SS4303T01 Online Replacement Guide DeltaV Maintenance

Emerson SS4303T01 Online Replacement Guide | DeltaV Maintenance

Is Online Replacement of the Emerson SS4303T01 Safe for Active Control Systems?

Industrial automation relies on continuous uptime. In modern DCS environments, the ability to maintain hardware without halting production is a critical operational requirement. The Emerson SS4303T01 module is a central component in DeltaV architectures. While engineers often discuss its “hot-swap” capabilities, successful online replacement requires a deep understanding of system redundancy and environmental risks. This article explores the technical nuances of servicing this hardware in live environments.

Emerson SS4303T01 Online Replacement Guide DeltaV Maintenance

Emerson SS4303T01 Online Replacement Guide DeltaV Maintenance

Understanding the Functional Role of the SS4303T01 in DCS

The SS4303T01 serves as a vital communication or power interface within the Emerson DeltaV ecosystem. It facilitates data flow between the controller and I/O subsystems. In high-stakes industries like oil and gas or pharmaceuticals, this module ensures that process variables reach the control logic without latency. Its design prioritizes high availability. However, the hardware works within a complex backplane. Therefore, its performance depends on the integrity of the entire carrier assembly.

The Mechanics of Redundancy and Hot-Swapping Logic

True hot-swapping is only possible when the system maintains a redundant state. Before you remove an active SS4303T01, you must verify that the secondary communication path is fully synchronized. If the redundant partner is offline or degraded, pulling the module will trigger a system trip. Active diagnostics tools in the DeltaV explorer provide real-time health checks. We recommend confirming “Good” status across all communication nodes. Moreover, you should check for “Standby Ready” indicators to ensure a seamless transition during the physical swap.

Evaluating Physical Risks During Online Maintenance

Physical factors often cause more failures than software logic. In older plants, the carrier connectors may suffer from oxidation or mechanical fatigue. Inserting a new module into a worn backplane can create intermittent “ghost” faults. These faults are difficult to troubleshoot because they appear randomly under different thermal loads. Additionally, electrostatic discharge (ESD) remains a silent killer of industrial electronics. Always use grounded wrist straps. As a result, you protect the sensitive CMOS components inside the replacement unit from latent damage.

Strategic Considerations

When sourcing specialized hardware like the SS4303T01, reliability is the primary keyword for procurement officers. Market data indicates that nearly 40% of unplanned downtime in factory automation stems from improper maintenance of aged components. Adhering to ISA environmental standards ensures your hardware lasts its full lifecycle. Furthermore, engineers should prioritize original equipment to avoid firmware mismatches. For high-quality components and expert technical support, professionals often turn to trusted distributors like Powergear X Automation Limited.

Operational Guidelines for Field Engineers

  • ✅ Pre-Maintenance Audit: Verify the redundancy synchronization status in the DeltaV Diagnostics shell.
  • ⚙️ Environmental Check: Ensure the cabinet temperature is within limits to prevent thermal shock to the new module.
  • 🔧 Mechanical Precision: Align the module carefully with the carrier guides to avoid bending backplane pins.
  • 📊 Post-Installation Monitoring: Observe the LED indicators and system logs for at least 15 minutes after the swap.

Expert Insight from Powergear X Automation Limited

At Powergear X Automation Limited, we have observed that many “module failures” are actually infrastructure issues. We suggest that maintenance teams inspect cabinet grounding every six months. Poor grounding creates electrical noise that mimics hardware faults. If you are looking to optimize your spare parts inventory or need guidance on legacy system compatibility, explore our comprehensive catalog at https://www.powergearx.com/ for reliable automation solutions.

Application Scenario: Refinery Distillation Column

In a refinery setting, a distillation column must run for years without interruption. If a communication module fails, the SS4303T01 allows the maintenance team to restore redundancy while the column remains in a steady state. By following a strict MOC (Management of Change) protocol, the team replaces the faulty unit during a scheduled “low-activity” shift. This strategy eliminates the risk of a $500,000 production loss associated with an emergency shutdown.

Frequently Asked Questions (FAQ)

Q1: Can I replace the module if the “Active” light is blinking?
A: A blinking light usually indicates a synchronization process or a diagnostic warning. You should never pull the module until the redundancy status is confirmed as “Stable” and “Standby” in the software.

Q2: Does the new module require a firmware download after insertion?
A: In most DeltaV versions, the controller automatically detects the hardware revision. However, if the version mismatch is significant, you may need to perform a “Partial Download” to align the firmware.

Q3: What is the biggest cause of failure after an online swap?
A: Most post-replacement failures are due to improper seating in the carrier or latent ESD damage. Ensure the module is firmly locked and that you are using proper anti-static procedures.

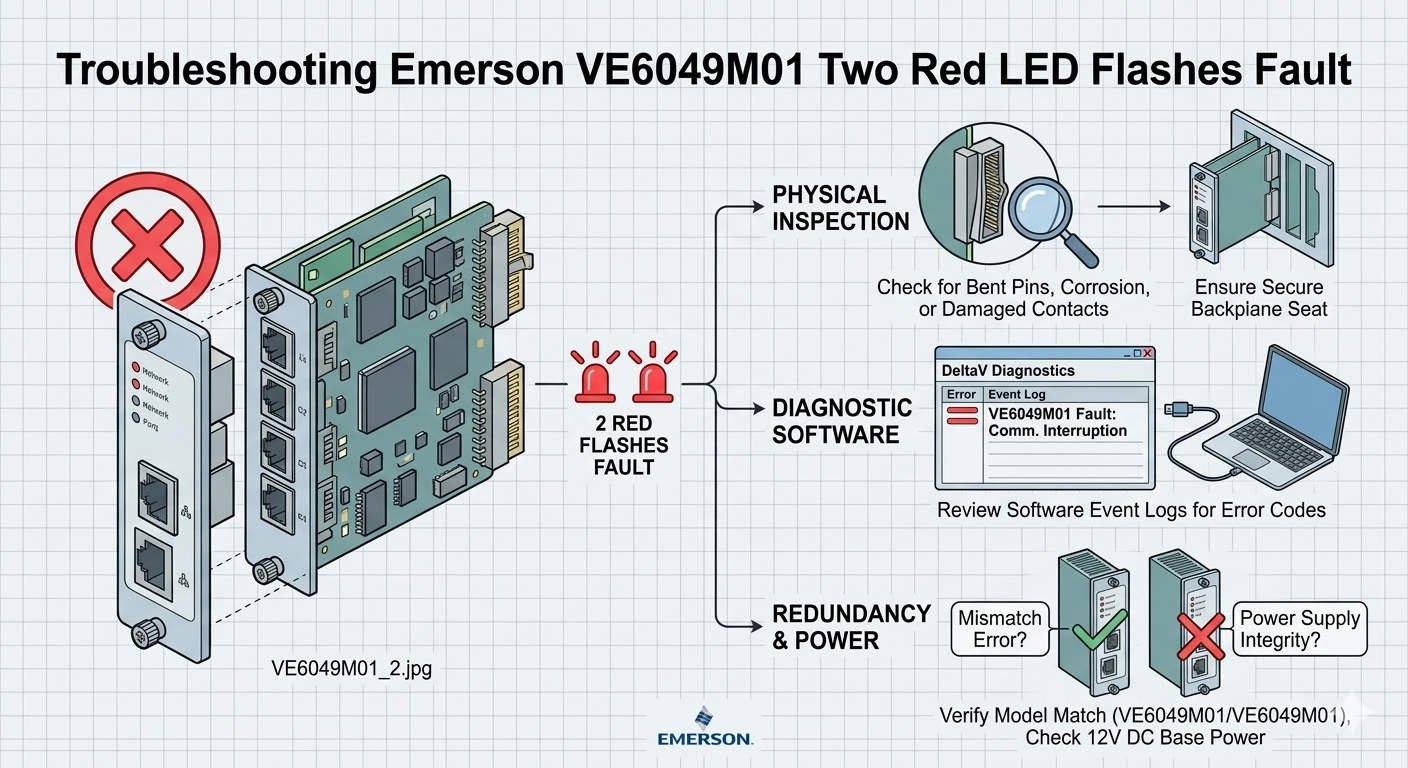
Troubleshooting Emerson VE6049M01 Two Red LED Flashes Fault

Troubleshooting Emerson VE6049M01 Two Red LED Flashes Fault

Troubleshooting the Emerson VE6049M01: Understanding the “Two Red LED Flashes” Fault

In the world of industrial automation, clear diagnostics save time and money. The Emerson VE6049M01 interface module serves as a critical link in the DeltaV DCS ecosystem. However, maintenance teams often encounter a specific fault signal: two repeating red LED flashes. This visual alarm indicates a hardware initialization failure or a self-test error. Understanding the root causes of this pattern helps engineers avoid unnecessary downtime in continuous-process environments.

Troubleshooting Emerson VE6049M01 Two Red LED Flashes Fault

Troubleshooting Emerson VE6049M01 Two Red LED Flashes Fault

The Functional Role of VE6049M01 in Factory Automation

The VE6049M01 provides essential communication between DeltaV controllers and I/O subsystems. It manages high-speed data exchange required for real-time control logic. As a result, any failure in this module can impact refinery safety or chemical batch quality. Industries such as oil & gas and power generation rely on this hardware for its high availability. The module translates complex electrical signals into actionable data for the DCS.

Technical Analysis of Initialization Faults and Power Stability

Voltage quality plays a decisive role in module startup. The VE6049M01 requires a clean 24VDC supply to initialize its internal logic successfully. Excessive ripple or transient sags during boot-up often trigger the two-flash red LED error. Standard multimeters might show a steady 24V reading. However, only an oscilloscope can reveal the high-frequency noise that disrupts sensitive electronics. Therefore, checking power quality is the first step in effective troubleshooting.

Backplane Integrity and Mechanical Communication Failures

Mechanical issues frequently mimic electronic hardware failures in industrial control systems. A two-flash red LED often signals that the module cannot communicate with the carrier backplane. Oxidation on gold edge connectors or bent pins can interrupt data packets. Moreover, constant vibration in compressor houses or offshore platforms may loosen the module seating. Engineers should inspect the physical connection before assuming the module is defective. Re-seating the module often clears the fault immediately.

Firmware Compatibility in Modern Distributed Control Systems

Compatibility issues often arise during phased plant modernization projects. Newer VE6049M01 hardware might not communicate correctly with legacy DeltaV software revisions. If the controller firmware does not recognize the module’s revision, the initialization self-test will fail. This mismatch presents as a persistent diagnostic alarm. Maintenance teams must verify the Emerson compatibility matrix before installing replacement units. Alignment between software and hardware ensures long-term system stability.

Best Practices for Installation and Maintenance

  • ✅ Verify Load Voltage: Test the 24VDC supply while the system is under full load.
  • ⚙️ Confirm Seating: Ensure the module clicks firmly into the carrier slot.
  • 🔧 Inspect Pins: Use a magnifying tool to check for bent or oxidized backplane connectors.
  • 📊 Check Software: Cross-reference firmware versions in the DeltaV explorer.

Expert Insights from Powergear X Automation Limited

At Powergear X Automation Limited, we observe that nearly 30% of “failed” modules are actually victims of poor infrastructure. Issues like grounding loops and aging power supplies create phantom faults. We recommend a “swap-test” method. Move the suspect module to a known-good carrier slot to isolate the problem. If the fault persists, only then should you proceed with procurement. For genuine Emerson components and technical consultation, visit our official site at https://www.powergearx.com/.

Application Scenario: Chemical Plant Power Disturbance

Consider a chemical plant experiencing intermittent “Two Red Flash” alarms on their VE6049M01 modules. After investigating, engineers found that large motor starts were causing momentary voltage sags. These sags didn’t trip the breakers but confused the module’s startup logic. By installing a dedicated power conditioner for the DeltaV cabinet, the plant eliminated the alarms. This solution saved thousands of dollars compared to replacing multiple interface modules.

Frequently Asked Questions (FAQ)

Q1: Does the “Two Red Flash” pattern always mean the hardware is broken?
A: Not necessarily. In our experience, this pattern frequently stems from external factors like backplane communication loss or poor power quality rather than internal circuitry failure.

Q2: Can I perform a hot-swap on the VE6049M01 while the process is running?
A: While DeltaV supports hot-swapping, you must first verify redundancy status. Pulling a module without a healthy backup can trigger a fail-safe shutdown of the entire I/O rack.

Q3: Why does the module work sometimes after a cold restart?
A: Initialization depends on timing and voltage levels. A cold restart might provide a slightly cleaner startup sequence, allowing the module to bypass a marginal self-test failure temporarily.

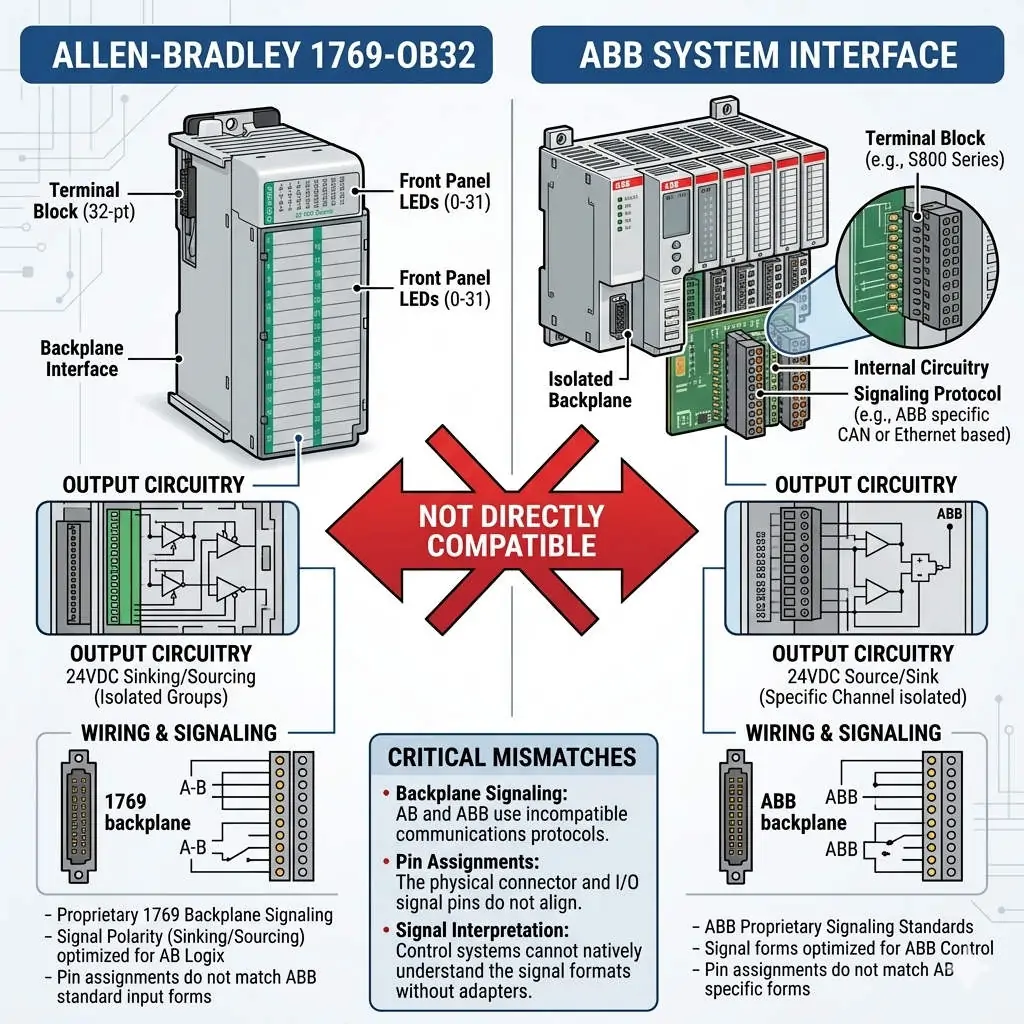
Why 1769-OB32 Is Not Directly Compatible with ABB Systems

Allen-Bradley 1769-OB32 Technical Guide: Features & Integration

Strategic Integration and Technical Analysis of the Allen-Bradley 1769-OB32 Digital Output Module

High-Density Control in Industrial Automation Ecosystems

The Allen-Bradley 1769-OB32 stands as a high-density digital output solution within the Rockwell Automation CompactLogix family. This module provides 32 solid-state 24V DC sourcing outputs in a single compact slot. Consequently, it excels in factory automation environments where control cabinet space is at a premium. By consolidating multiple output points, engineers can drive relays, solenoids, and small actuators with maximum efficiency. However, its performance remains intrinsically linked to the Rockwell proprietary backplane architecture.

Why 1769-OB32 Is Not Directly Compatible with ABB Systems

Why 1769-OB32 Is Not Directly Compatible with ABB Systems

Technical Mechanics: Sourcing Outputs and Backplane Dynamics

The 1769-OB32 utilizes a sourcing (PNP) logic configuration, which is the standard for North American industrial automation. Each output point delivers current to the field load, requiring a common ground for the circuit. In addition, the module features a typical response time of less than 1 millisecond. This speed is vital for high-speed packaging and sorting systems. Nevertheless, this hardware relies on the 1769 bus protocol for data exchange. This proprietary communication ensures sub-millisecond synchronization within a CompactLogix rack but creates a barrier for non-Rockwell systems.

Addressing Cross-Platform Compatibility Challenges

A frequent engineering query involves connecting the 1769-OB32 to ABB control systems like the AC500 or 800xA. In practice, direct physical integration is impossible due to incompatible backplane buses and communication protocols. While ABB might support EtherNet/IP, the physical 1769 interface is exclusive to Allen-Bradley. To bridge this gap, engineers often deploy industrial gateways (e.g., EtherNet/IP to PROFINET). However, this method introduces latency and increases system complexity. Therefore, Powergear X Automation Limited recommends using native ABB I/O modules for ABB-centric projects to ensure long-term stability.

Installation Standards and Maintenance Best Practices

Field experience suggests that proper protection is essential for maximizing the lifespan of the 1769-OB32. Inductive loads, such as large solenoids, can generate significant back-EMF during switching. To mitigate this risk, follow these technical guidelines:

  • ✅ Surge Suppression: Install flyback diodes or RC snubbers across inductive loads to prevent output point damage.
  • ✅ Grounding Protocols: Use shielded cables for long-distance runs and implement single-point grounding to reduce EMI.
  • ✅ Power Quality: Deploy 24V DC surge protective devices (SPD) in environments prone to lightning or heavy motor interference.
  • ✅ Wiring Integrity: Ensure the 18-point removable terminal block (RTB) is securely seated to avoid intermittent connectivity.

Strategic Procurement: Assessing Total Cost of Ownership

From a buyer’s perspective, the 1769-OB32 is a high-value asset primarily when maintaining an existing Rockwell infrastructure. According to MarketsandMarkets, the global PLC market is shifting toward unified ecosystems to reduce downtime. Mixing I/O brands often leads to “hidden costs” in the form of specialized spare parts and extended troubleshooting hours. If your primary DCS is ABB, replacing 1769 modules with native S500 or S800 series I/O is usually the more cost-effective strategy over the machine’s lifecycle.

Expert Commentary from Powergear X Automation Limited

At Powergear X Automation Limited, we emphasize that the 1769-OB32 is a specialized component, not a generic universal tool. It represents the pinnacle of compact sourcing output technology for the CompactLogix range. While communication integration via gateways is technically feasible, it is rarely the most “elegant” engineering solution. We advise our clients to prioritize platform homogeneity. This approach minimizes “MTTR” (Mean Time To Repair) and simplifies the training requirements for plant floor technicians.

Application Scenarios and Practical Solutions

  • Automotive Assembly: Managing 32-point valve banks for pneumatic clamping systems in high-speed robot cells.
  • Discrete Manufacturing: Controlling small DC motor starters and signal indicators in compact control panels.
  • Legacy Migrations: Acting as a high-density replacement during upgrades of older SLC 500 systems to CompactLogix.

Frequently Asked Questions (FAQ)

Q: Can I mix NPN sensors with the 1769-OB32 sourcing outputs?
Direct connection is not possible because the 1769-OB32 provides current (PNP) while NPN sensors expect a sinking input. You must use intermediate relays or signal converters to bridge the two different logic types.

Q: What is the primary cause of individual output point failure on this module?
The most common cause is an overcurrent condition or a short circuit in the field wiring. Since these are solid-state outputs, a single high-voltage spike from an unprotected solenoid can permanently damage the switching transistor for that specific channel.

Q: Is it better to use a gateway or replace the module when switching to an ABB controller?
Unless the 1769-OB32 is part of a large, pre-existing rack that cannot be moved, replacing it with native ABB I/O is the superior choice. Gateways add a “point of failure” and increase communication jitter, which can affect precision timing.

To discover more high-performance modules and expert automation advice, please visit the official Powergear X Automation Limited website for our latest inventory and technical support.

Clear 1769-L32E Major Faults: Expert PLC Troubleshooting Guide

Clear 1769-L32E Major Faults: Expert PLC Troubleshooting Guide

Mastering Major Fault Recovery for the Allen-Bradley 1769-L32E CompactLogix

The 1769-L32E serves as a cornerstone in modern industrial control. This EtherNet/IP-enabled controller bridges the gap between small-scale logic and complex integrated systems. However, encountering a “Major Fault” can bring production to a standstill. Understanding the mechanics behind these errors is vital for any field engineer aiming to minimize downtime and maintain system integrity.

Clear 1769-L32E Major Faults: Expert PLC Troubleshooting Guide

Understanding the Mechanics of Controller Fault States

A Major Fault transitions the 1769-L32E into a halted state to protect hardware and personnel. During this mode, the controller stops executing user logic and sets outputs to their configured “Safe State.” This immediate shutdown is critical in high-speed packaging or chemical processing where erratic behavior could be catastrophic. Active monitoring via the status LEDs provides the first clue; a flashing red “OK” light typically indicates a recoverable major fault.

The Role of CompactFlash in System Recovery

The 1769-L32E utilizes CompactFlash (CF) non-volatile memory for robust program retention. While this ensures the controller recovers after power loss, it can create a “fault loop.” If the CF card contains a corrupted image or a program with an inherent logic error, the controller will reload that error every time it boots. Therefore, engineers must verify the “Load Image” settings in RSLogix 5000 before initiating a cold restart on-site.

Strategic Troubleshooting Procedures in the Field

Restoring a faulted system requires a disciplined, step-by-step approach to identify the root cause rather than just clearing the symptom. Follow this validated workflow to ensure long-term stability:

  • Step 1: Establish a connection using Studio 5000 or RSLogix 5000 software.
  • Step 2: Navigate to the Controller Properties and select the Major Faults tab.
  • Step 3: Record the Fault Type and Code (e.g., Type 04, Code 31 for an index out of range).
  • Step 4: Address the hardware failure or modify the offending rung of logic.
  • Step 5: Clear the fault in the software and return the key switch to Run Mode.

Identifying Common Hardware and Communication Triggers

External factors often trigger internal logic faults. In the industrial automation sector, electrical noise remains a primary culprit for backplane instability. According to IEEE standards, improper grounding can lead to intermittent communication losses. When the 1769-L32E loses contact with a critical I/O module, it may trigger a Major Fault to prevent the process from running blindly. High-vibration environments can also loosen terminal blocks, leading to module connection timeouts.

Expert Insights from Powergear X Automation Limited

At Powergear X Automation Limited, we observe that many “unexplained” faults stem from aging power supplies or firmware mismatches. As these controllers approach their end-of-life cycle, the internal capacitors may degrade. We recommend a proactive migration strategy for units exceeding ten years of service. Standardizing your firmware versions across the plant floor is also essential. This practice reduces the risk of unexpected instruction behavior during routine maintenance or part replacement.

Advanced Selection: When to Repair or Replace

Choosing between troubleshooting and replacement depends on the frequency of the errors. If a 1769-L32E experiences recurring non-recoverable faults (Solid Red LED), the internal circuitry likely has permanent damage. In such cases, replacing the unit is more cost-effective than risking a multi-day outage. For new installations, always ensure your choice aligns with the I/O count and memory requirements of your specific application.

Typical Solution Scenarios

  • Water Treatment Skids: Using the 1769-L32E for PID control and remote telemetry over EtherNet/IP.
  • Material Handling: Managing high-speed sorters where localized I/O processing is required.
  • Automotive Assembly: Integrating with various sensors and actuators via the 1769 backplane.

Frequently Asked Questions (FAQ)

1. Why does my controller fault immediately after I clear it?
This usually happens because the trigger—such as a “Divide by Zero” error or an array overflow—is still present in your logic. The controller re-executes the bad code the moment it enters Run Mode. You must fix the math or logic constraints before resetting.

2. Can I clear a major fault without using a laptop or software?
In some cases, toggling the physical key switch from Run to Program and back to Run can clear minor recoverable faults. However, for a Major Fault, a power cycle or software intervention is typically required to ensure the cause is acknowledged.

3. How does electrical noise specifically cause a Major Fault?
High-frequency noise from VFDs can corrupt data packets on the backplane. If the controller receives “garbage” data where it expects a module heartbeat, it assumes a hardware failure and enters a fault state to maintain safety.

For more technical support and high-quality industrial components, visit the experts at Powergear X Automation Limited today.

1769-IQ16 Troubleshooting: LED ON but No PLC Input Status Guide

1769-IQ16 Troubleshooting: Why the LED is ON but the PLC Program is OFF

In the world of factory automation, few things are as frustrating as a “lying” LED. You see the green light on your input module, yet the controller tags remain stubbornly at zero. This specific issue with the 1769-IQ16 digital input module often leads to unnecessary hardware replacements. Understanding the gap between physical electrical signals and digital logic is essential for any field engineer working with CompactLogix systems.

1769-IQ16 Troubleshooting: LED ON but No PLC Input Status Guide

Understanding the 1769-IQ16 Logic Threshold Gap

The 1769-IQ16 is a 16-point sinking/sourcing 24V DC input module. However, a common misconception is that any voltage will trigger a logical “1” in the PLC. While the LED may glow at lower voltages, the internal optoisolator requires a specific threshold to register. According to industry standards for industrial automation, most 24V modules require at least 10V to 15V to guarantee an “ON” state. If your sensor provides a weak 8V signal due to high impedance or long cable runs, the LED might illuminate faintly while the PLC remains blind to the input.

The Hidden Impact of Input Filter Settings

Digital filtering is a core feature of the 1769-IQ16. It prevents “contact bounce” from mechanical switches, which can cause erratic logic execution. However, if the filter time is set to 20ms for a high-speed sensor pulse lasting only 5ms, the PLC will ignore the signal. Engineers often overlook this software configuration during control systems commissioning. Therefore, you must match the filter constant to the specific speed of your field device to ensure data integrity in factory automation environments.

Common Wiring Pitfalls: The Sinking vs. Sourcing Conflict

Incorrect common (COM) wiring is the most frequent cause of signal loss. The 1769-IQ16 allows for flexible wiring, but mixing PNP (Sourcing) and NPN (Sinking) sensors on the same common group leads to failure. In many DCS or PLC applications, a “floating” common will allow enough leakage current to light the module’s LED, but it lacks the current drive to trigger the internal logic. You should always use a high-quality multimeter to verify the potential difference between the input terminal and the specific group common.

Backplane Communication and I/O Mapping Errors

Sometimes the hardware is perfect, but the software bridge is broken. If the module is not correctly defined in the Studio 5000 I/O configuration, or if a “Generic Profile” is used incorrectly, the data will not update. Moreover, a “Major Fault” on a different module in the same 1769 backplane can occasionally freeze I/O updates for the entire rack. We recommend always using the latest Add-On Profiles (AOP) from the manufacturer to ensure seamless integration and E-E-A-T compliance in your system documentation.

Strategic Technical Insights from Powergear X Automation Limited

At Powergear X Automation Limited, we have observed that roughly 40% of reported “module failures” are actually environmental or configuration issues. As PLC technology evolves toward IIoT, signal integrity becomes even more critical. We suggest implementing shielded twisted-pair cabling for any input runs exceeding 30 meters to combat electromagnetic interference. If you are looking to optimize your spares inventory or need expert guidance on high-reliability control modules, explore the comprehensive solutions at Powergear X Automation Limited.

Technical Checklist for Field Maintenance

  • ✅ Voltage Verification: Ensure the input voltage at the terminal is ≥ 15V DC during the “ON” state.
  • ✅ Common Continuity: Confirm the return path (COM) is securely landed and matches the sensor type.
  • ✅ Filter Audit: Check the Module Properties in software to ensure filter times don’t exceed pulse widths.
  • ✅ Tag Monitoring: Use the “Monitor Tags” feature in the PLC software rather than relying on HMI animations.
  • ✅ Firmware Check: Verify that the module revision matches the project configuration to avoid “Electronic Keying” mismatches.

Industrial Application Scenarios

The 1769-IQ16 excels in diverse sectors. In Oil & Gas, it monitors valve position limits where reliability is non-negotiable. In the Pharmaceutical industry, it tracks high-speed bottling sensors where precise filter timing is the difference between a successful batch and a rejected one. As a result, mastering the troubleshooting of this module is a core competency for any field engineer.

Frequently Asked Questions (FAQ)

1. Can I use the 1769-IQ16 with AC signals?
No, this is a DC-only module. Attempting to use AC will likely damage the internal circuitry or result in high-frequency flickering that the PLC cannot process.

2. Why does my input stay “ON” in the program even after I disconnect the wire?
This is often caused by “Input Forcing” being active in the software or a program routine that “latches” the bit. Always check the “Forced” column in your controller tags.

3. Is it possible for a single channel to fail while the others work?
Yes. Optoisolators can fail due to localized overvoltage or short circuits. If you have a spare channel, move the wire and update the address in your code to quickly restore production.

For high-quality automation hardware and expert technical support, visit the specialists at Powergear X Automation Limited today.

Back to Top
Product has been added to your cart